Global Steel Supply & Processing
Specify Q690D quenched-and-tempered high-strength structural plate to GB/T 16270-2009. Compare the correct thickness-specific yield and tensile band, −20°C Charpy performance, heat CEV and production documentation before requesting a bulk quote.
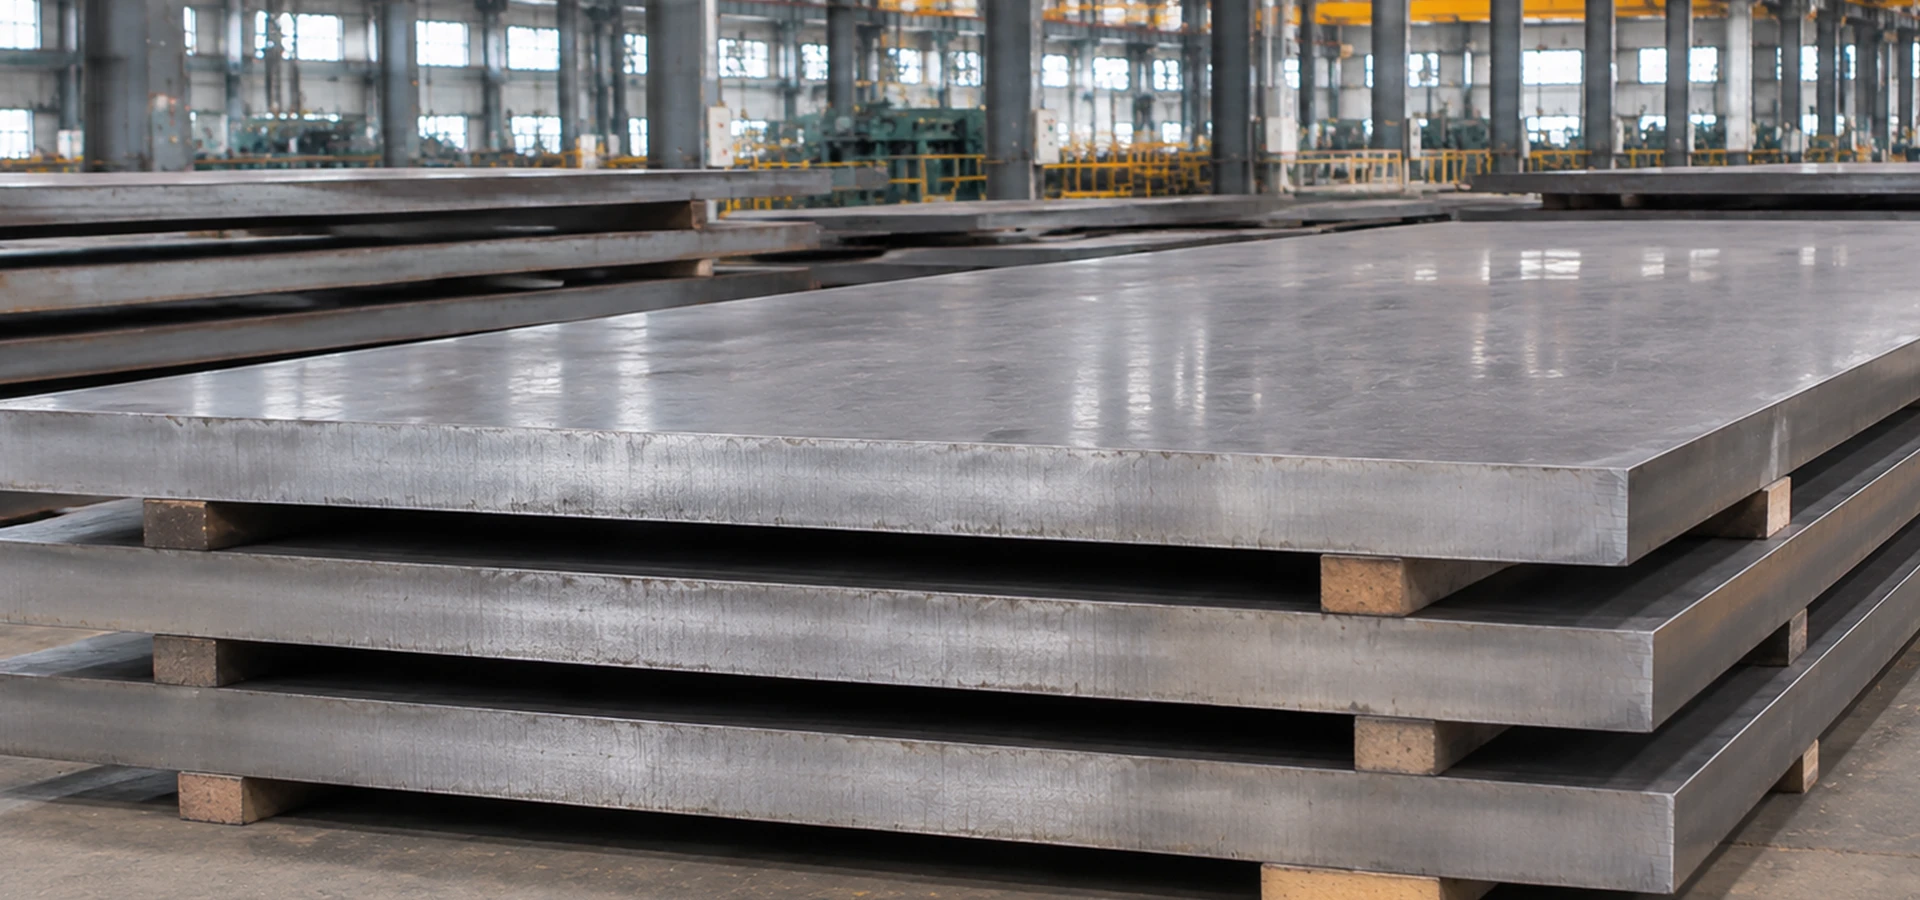
This page covers Q690D high-strength plate supplied in quenched-and-tempered condition under GB/T 16270-2009. Its 690 MPa grade designation applies to the first thickness band; use the relevant strength limits for heavier plates.
| Purchase field | What to specify / verify |
|---|---|
| Product identity | Q690D high-strength structural steel plate; D quality level; quenched and tempered condition. |
| Governing steel-plate standard | GB/T 16270-2009, not a hot-rolled sheet or section specification. Confirm the standard and grade on the purchase order and MTC. |
| Mechanical-property coverage | Plate thickness up to 150 mm is covered in three mechanical-property bands by the standard. Actual stock and source-mill rolling / Q&T size capability must be confirmed. |
| Delivery condition | Quenched and tempered (Q&T), with finished mechanical and Charpy properties verified for the specified plate thickness. |
| Yield strength | 690 MPa through 50 mm; 650 MPa above 50 to 100 mm; 630 MPa above 100 to 150 mm. |
| Tensile strength | 770–940 MPa at ≤50 mm; 760–930 MPa at >50–100 mm; 710–900 MPa at >100–150 mm. |
| Charpy toughness | −20°C; 47 J minimum average longitudinal Charpy V-notch energy for full-size samples. Reduced-size specimen provisions apply to thinner steel plate. |
| Carbon equivalent | Maximum CEV 0.65% through 50 mm; 0.77% above 50–100 mm; 0.83% above 100–150 mm. |
| Dimensional requirement | Specify thickness × width × length, tolerances under GB/T 709, flatness, plate marking and quantity. |
| Supporting documents | MTC including producer, standard, heat analysis, CEV, mechanical results, −20°C impact records, Q&T state and any agreed additional inspection. |
Q690D has three separate tensile ranges across the standard thickness bands. The 690 MPa minimum yield figure applies through 50 mm, while heavier plate uses 650 MPa or 630 MPa as specified below.
| Plate thickness | Min. yield (MPa) | Tensile (MPa) | Min. elongation |
|---|---|---|---|
| ≤50 mm | 690 | 770–940 | 14% |
| >50–100 mm | 650 | 760–930 | 14% |
| >100–150 mm | 630 | 710–900 | 14% |
Values are from GB/T 16270-2009, Table 2, for Q690D Q&T plate. Transverse tensile specimens and longitudinal impact specimens are used. The actual mill certificate records heat-specific measured results; thickness up to 150 mm is a standards scope, not a guaranteed stock range.
Send the full plate schedule and working thickness range. We will check the producer’s Q&T route, mill certificate and available shipment lots.
Maximum heat-analysis limits for Q690D under GB/T 16270-2009 Table 1. Actual alloy additions vary by mill practice; optional Cu, Cr, Ni, Mo, B, V, Nb and Ti maxima are ceilings, not universal nominal compositions.
| Element | Max. content (%) |
|---|---|
| C | 0.20 |
| Si | 0.80 |
| Mn | 1.80 |
| P | 0.025 |
| S | 0.015 |
| Cr | 1.50 |
| Ni | 2.00 |
| Element | Max. content (%) |
|---|---|
| Cu | 0.50 |
| Mo | 0.70 |
| V | 0.12 |
| Nb | 0.06 |
| Ti | 0.05 |
| B | 0.0050 |
| Nominal thickness | Maximum CEV | Procurement use |
|---|---|---|
| ≤50 mm | 0.65% | Include heat-specific CEV in the WPS review. |
| >50–100 mm | 0.77% | Review preheat and hydrogen control for the actual section. |
| >100–150 mm | 0.83% | Validate heavier-section weld procedure and toughness. |
CEV = C + Mn/6 + (Cr + Mo + V)/5 + (Ni + Cu)/15. The standard requires grain refinement using at least one of Nb, Ti, V or Al to its stated threshold. Ask for the heat analysis and CEV calculation on the actual certificate; CET can be separately agreed in the purchase contract.
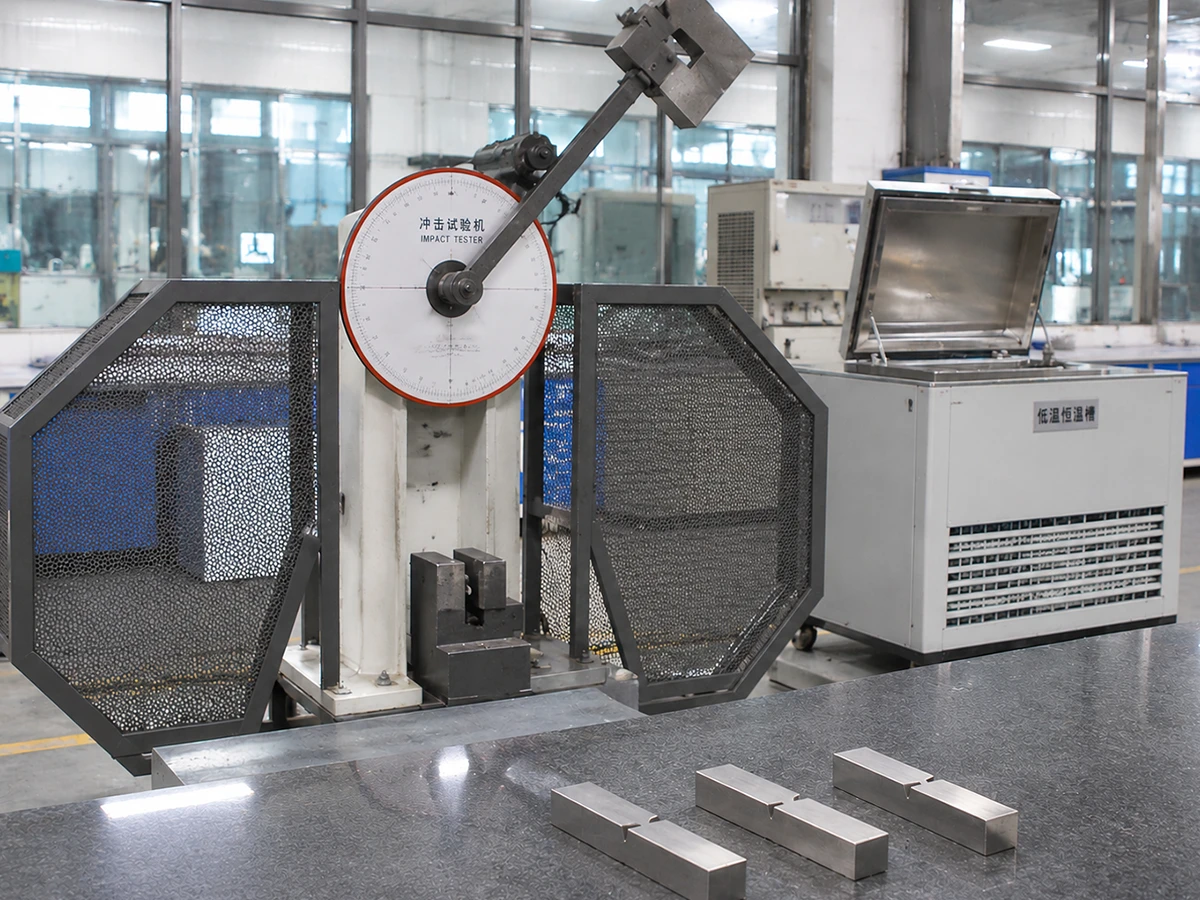
For Q690D to GB/T 16270-2009, the longitudinal Charpy V-notch impact requirement is 47 J average at −20°C for full-size specimens. Confirm sampling rules and reduced-size testing at lower thicknesses.
D quality level is tested at −20°C for the baseline Charpy requirement.
Minimum average longitudinal absorbed energy for full-size V-notch specimens.
For thickness below 12 mm, check reduced-size specimen and adjusted acceptance rules; plates below 6 mm do not undergo this Charpy test under the stated standard.
Specify −20°C and 47 J where applicable, plus sample orientation, plate thickness, extra low-temperature tests and witnessing requirements.
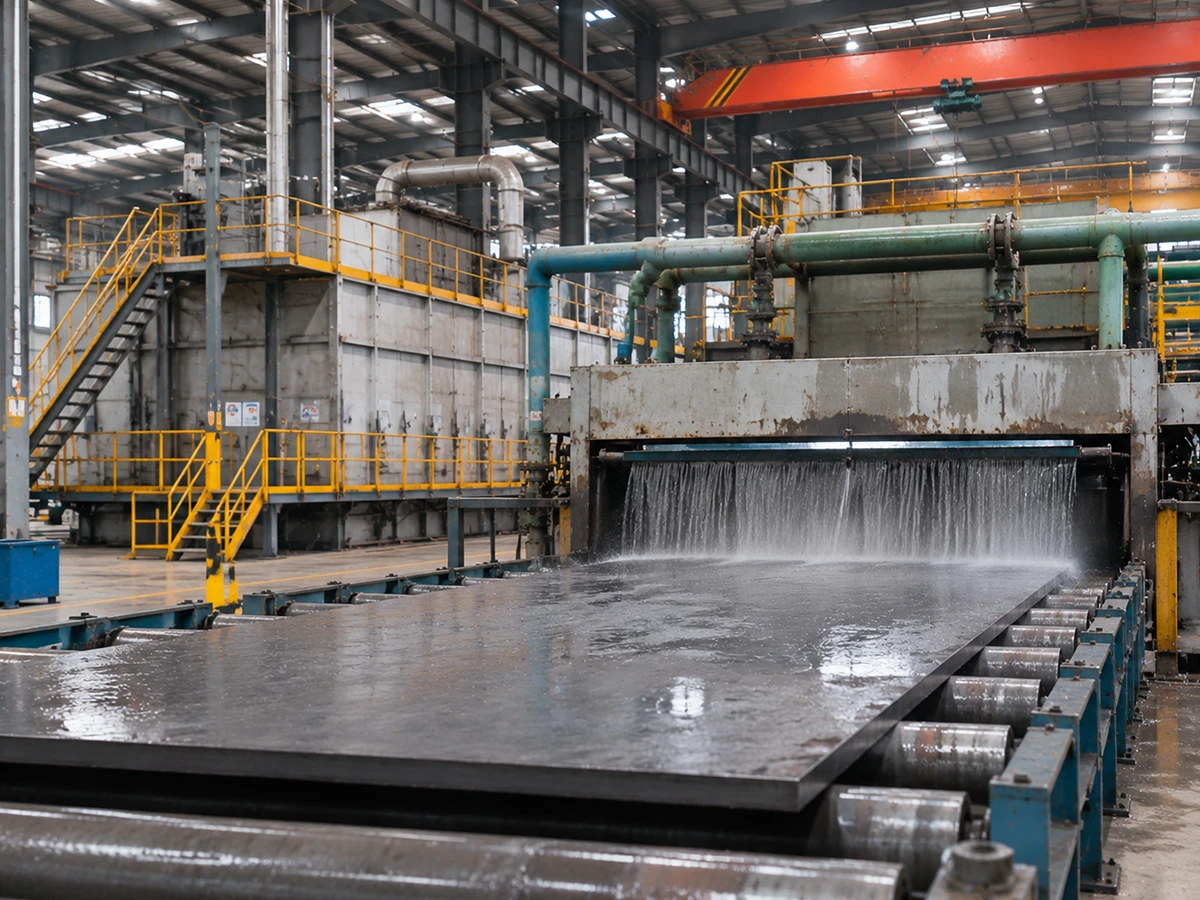
Q690D is supplied quenched and tempered under GB/T 16270-2009. The verified heat-treatment condition and finished plate testing are critical for thick-section tensile performance and weldable structural fabrication.
The mill uses controlled quenching and tempering to achieve the ordered high-strength/toughness combination. Specify the required plate dimensions, Q&T condition, heat traceability and documented impact performance before fabrication planning.
Q690D Q&T plate can be specified for weight-sensitive, highly loaded welded structural components where the design requires the Q690D strength and the −20°C impact level. Selection belongs to the project engineer and a qualified fabrication procedure.
Load-bearing boom boxes, lifting attachments and support sections selected for their verified thickness-specific strength and fatigue design.
Welded frames and highly loaded machine supports where the engineering drawing identifies Q690D Q&T plate and an approved welding sequence.
Plate parts for lifting equipment with documented heat input, member stability and inspection requirements.
Highly loaded chassis and main structural frames; abrasion-facing liners should be evaluated against a wear-plate standard.
Selected trailer, equipment-carrier and loading-support parts that require a qualified design and weld procedure.
Project-specific box beams, brackets and supports where the actual plate thickness band and accepted material standard are stated.
A 690 MPa grade designation alone does not justify reducing plate thickness or substituting other steel. Validate buckling, stiffness, fatigue, weldability, applicable code and the heat-specific MTC. Q690D structural plate is not a pressure-vessel or abrasion-resistant grade.
For Q690D orders, verifying the strength band and heat-treatment route before purchasing protects the drawing, fabrication schedule and material traceability.
Confirm GB/T 16270-2009, the Q690D D-class suffix, plate thickness, Q&T delivery and −20°C Charpy requirement together.
Check the producing mill, available thickness and plate dimensions, tested condition and current lot quantity before making a supply commitment.
Coordinate heat-by-heat tensile, impact, chemistry and CEV results, with supplementary inspection when written into the purchase order.
Align plate marks, cutting list, documents, packaging and shipping terms with your production and delivery schedule.
BAOSTEEL METAL company-wide profile: annual output 8 million MT, regular inventory 1 million MT, 500,000 m² operating area and 1,000+ employees. These figures describe the whole business, not Q690D-specific production, stock or source-mill approval.
Q690D supply involves high-strength plate rolling, quenching and tempering, and verified tensile and toughness testing. Confirm the producing steelworks, thickness capability, plate size, mill certificate and actual availability before allocating the order.
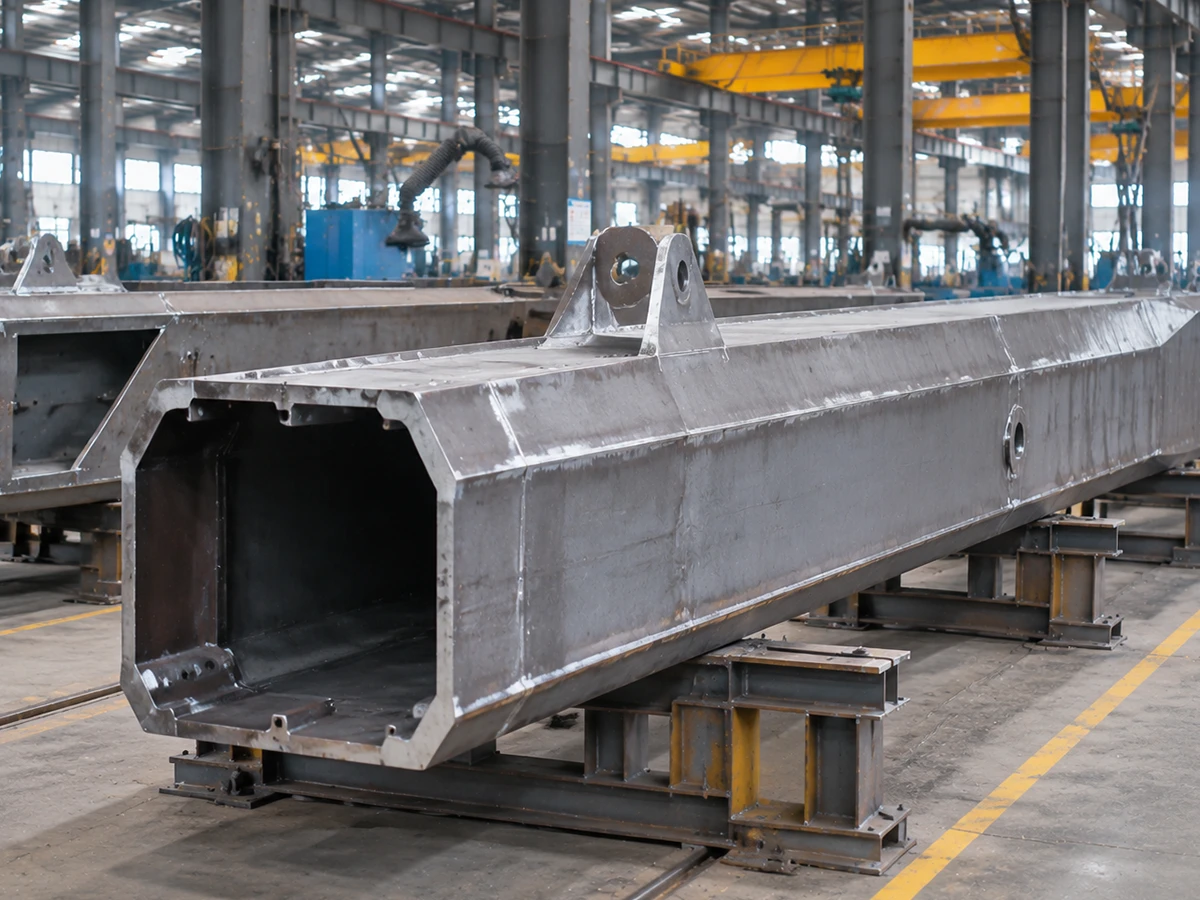
Match each heat/plate identity to the Grade Q690D Q&T material specification, its thickness-specific strength range, −20°C impact record and applicable supplementary inspection.
| Purchase field | What to specify / verify |
|---|---|
| Material identity | Q690D Q&T plate, GB/T 16270-2009, source steelworks and production heat. |
| Heat number | Matching heat / plate identification and ordered dimensions. |
| Chemistry | Heat analysis, P/S limits, fine-grain additions and CEV checked against the ordered thickness band. |
| Tensile tests | Transverse tensile results for the ordered thickness band: yield, the applicable tensile range and elongation A ≥14%. |
| Impact tests | Longitudinal Charpy results at −20°C, specimen dimensions, individual energy values and frequency. |
| Heat treatment | Quenching and tempering status; obtain treatment reports if specified in the contract. |
| Optional checks | UT acceptance, Z-direction quality, dimensional inspection and third-party witnessing only when agreed. |
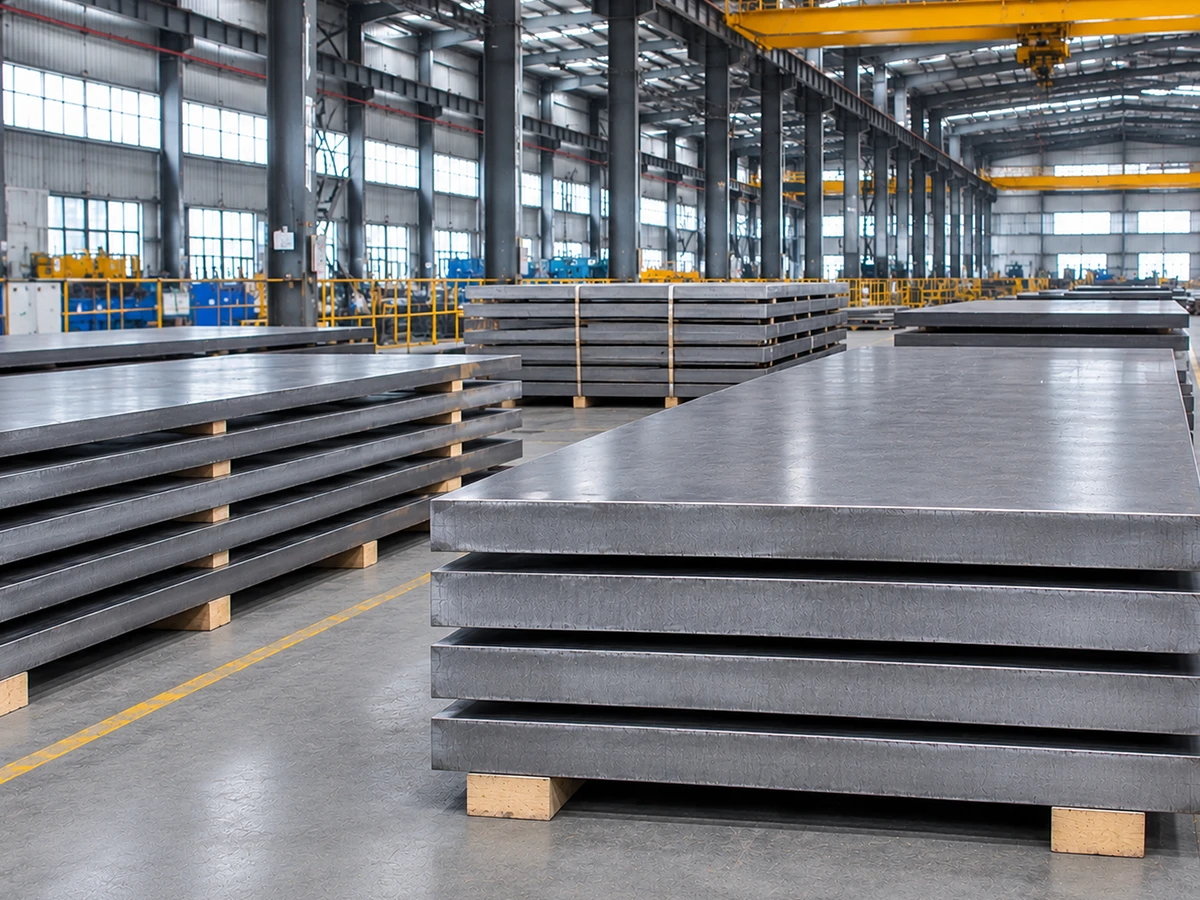
Specify the test method, acceptance level, sampling frequency, certificate format and any nominated inspection agency.
Q690D Q&T plate requires a qualified welding procedure suited to actual heat CEV, section thickness, restraint, consumables, hydrogen control and heat-affected-zone performance. Preheat and heat input must be determined from the joint and procedure—not a universal number.
Include nominal and cut dimensions, finished thickness, flatness, surface quality and plate marking on the Q690D schedule. The source mill confirms available sizes in the requested Q&T condition.
Choose the actual finished thickness band, tolerance class and flatness criterion. Dimensional tolerances can reference the ordered GB/T 709 edition where applicable.
Specify mill or cut edges, identification marks, surface acceptance, corrosion protection and shipping supports appropriate to heavy plates.
Calculate theoretical Q690D plate mass from the requested sizes and number of pieces using a planning density of 7,850 kg/m³.
Formula: thickness × width × length × 7.85 × 10⁻⁶ = kg per plate (dimensions in mm). Multiply by quantity; divide kg by 1,000 for metric tonnes.
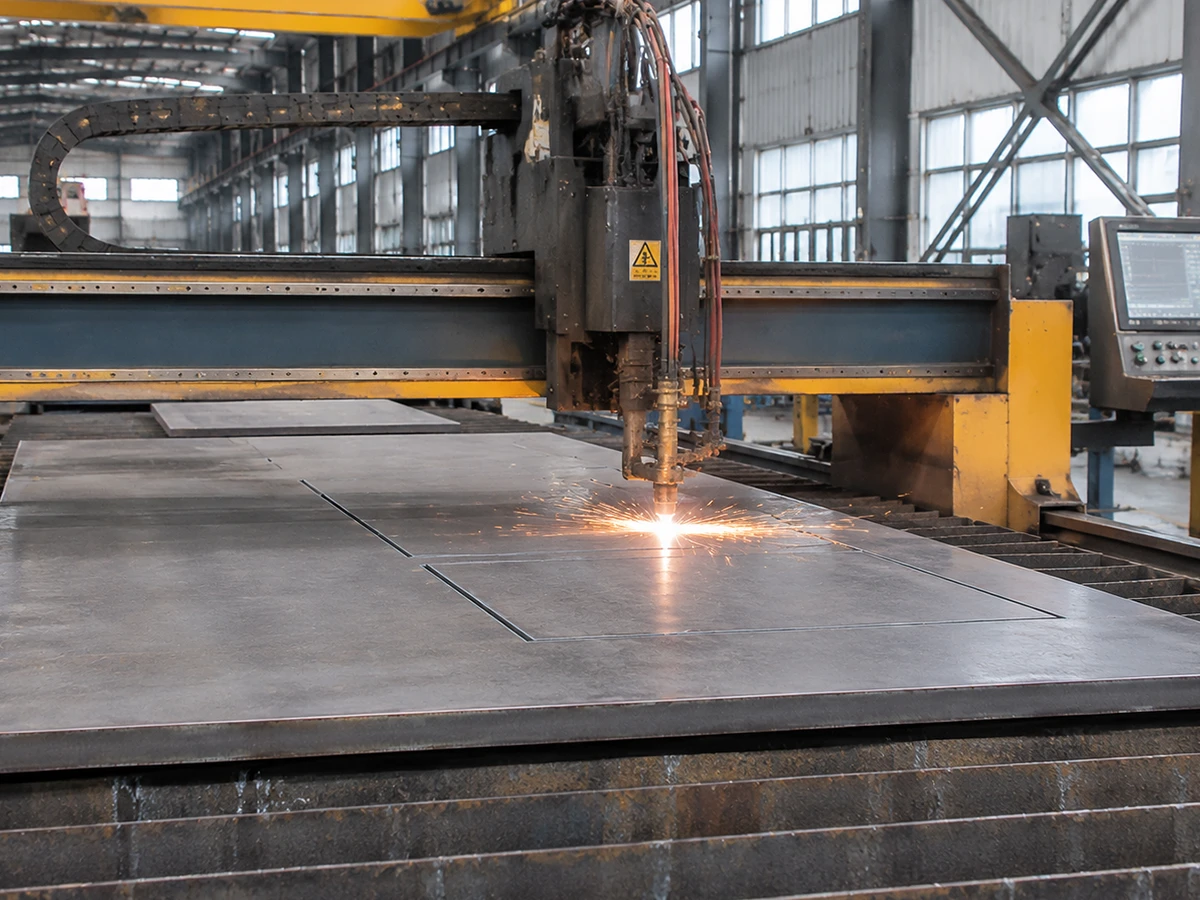
Include piece quantities, finished sizes, drawing revisions, tolerances, required edge quality and heat-number transfers.
Processing is offered subject to thickness, steel condition, drawing and workshop capacity; the resulting parts retain the original material heat identity.
Review kerf, thermal effects and dimensional allowance for Q&T high-strength plate.
Where plate thickness and equipment permit, evaluate CNC laser or alternative cutting technology.
Agree bevels, holes, marking and any extra inspection needed after processing.
Thermal cutting and subsequent forming can change local properties. The purchaser’s fabricator should approve the procedure for the relevant part design, plate thickness and Q&T condition.
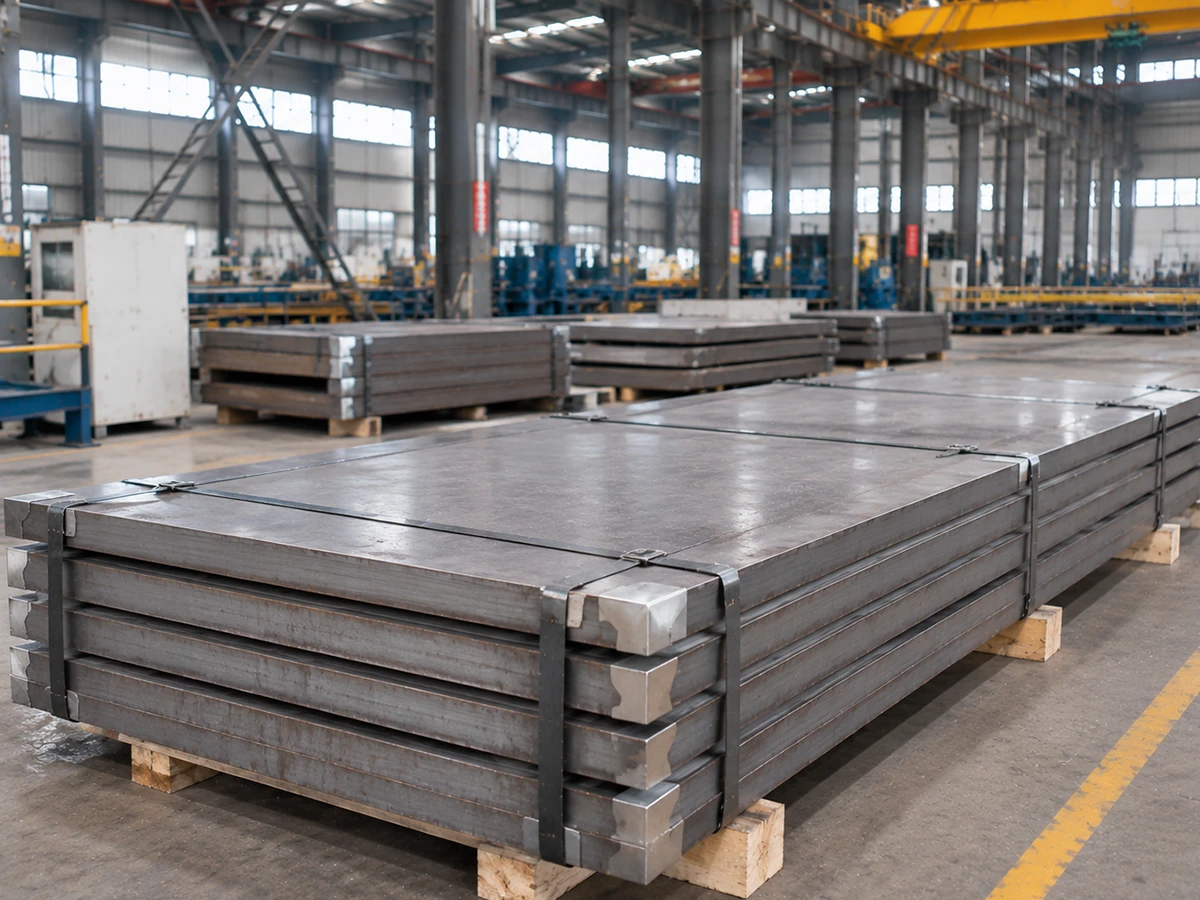
Order execution includes steel plate identification, matching documents, stable handling and agreed transport terms. Packaging is selected around the actual plate dimensions and route.
Browse adjacent structural strength grades and material systems. Each comparison requires the design authority to review standard, delivery condition, impact temperature, thickness and welding route.
GB/T 16270 Q&T 460 MPa class with its own thickness limits and C-level 0°C impact requirement.
Previous high-strength grade, with a separate 550 MPa thickness class and −20°C / 47 J impact requirement.
EN 10025-6 Q&T steel plate with distinct chemistry, impact level and inspection conditions; assess under the project design standard.
ASTM Q&T structural plate; strength, toughness, chemistry and thickness rules are not automatic substitutes for Q690D.
Same nominal 690 MPa family, with 0°C / −40°C / −60°C impact-temperature routes and different energy requirements.
Lower-strength ASTM structural steel, useful for comparing specification systems—not for automatic grade substitution.
Related grades are given for procurement comparison. Add internal hyperlinks only to live WordPress pages; a replacement grade requires project engineering approval.
Reference the exact grade, D-level impact and Q&T heat treatment. Add inspection acceptance levels and delivery terms before confirming the purchase.
Q690D is quenched-and-tempered high-strength structural steel plate to GB/T 16270-2009. The D quality suffix identifies a −20°C Charpy test route with 47 J minimum longitudinal average for full-size specimens.
The specified route is GB/T 16270-2009 for Q&T steel plates up to 150 mm under the standard. Other products described as Q690D may have a different material standard; check the certificate.
No. The minimum yield is 690 MPa through 50 mm, 650 MPa above 50–100 mm and 630 MPa above 100–150 mm under GB/T 16270-2009.
The standard specifies 770–940 MPa at ≤50 mm, 760–930 MPa at >50–100 mm, and 710–900 MPa at >100–150 mm. Minimum elongation A is 14%.
D-grade Q690D has a 47 J average minimum longitudinal V-notch impact requirement at −20°C for full-size test specimens. Reduced-size rules apply to eligible thin plates.
Yes, for Q690D ordered to GB/T 16270-2009 the plate is supplied in quenched-and-tempered condition. Request the Q&T identification, heat number and supporting test results from the producing mill.
Maximum CEV values are 0.65% through 50 mm, 0.77% above 50–100 mm and 0.83% above 100–150 mm. Welding decisions depend on actual heat chemistry, joint geometry, thickness and procedure qualification.
These are separate grade and standard systems. They differ in chemical limits, thickness-dependent properties, toughness and acceptance rules. Any substitution requires the design authority’s written approval.
Cutting and marking can be discussed against the drawing, original heat identity and applicable workshop capacity. Review thermal-cutting effects, edge preparation and any subsequent welding procedure.
Send GB/T 16270-2009, grade Q690D, full plate sizes, total tonnes, Q&T condition, −20°C impact requirements, chemistry/CEV, material documents, any UT or third-party inspection, destination and Incoterm.
Send GB/T 16270-2009 Q690D, thickness × width × length, total tonnage, Q&T and −20°C Charpy requirements, material-document scope, CEV limits, optional cutting and destination. We confirm the actual supplying mill and available lot before quotation.
Send your required grade, dimensions, quantity and destination. Our team will review the inquiry.
