Global Steel Supply & Processing
Source 09MnNiDR low-alloy steel plate for pressure equipment requiring verified low-temperature impact performance. Source to GB/T 713.3-2023 with nickel-alloyed chemistry, thickness-specific strength, normalized delivery and heat-traceable Charpy records.
The grade-standard thickness is 6–120 mm. For plate above 80 mm, the base Charpy test is −60°C / 60 J. Actual sizes, stock and delivery are confirmed by mill and order.
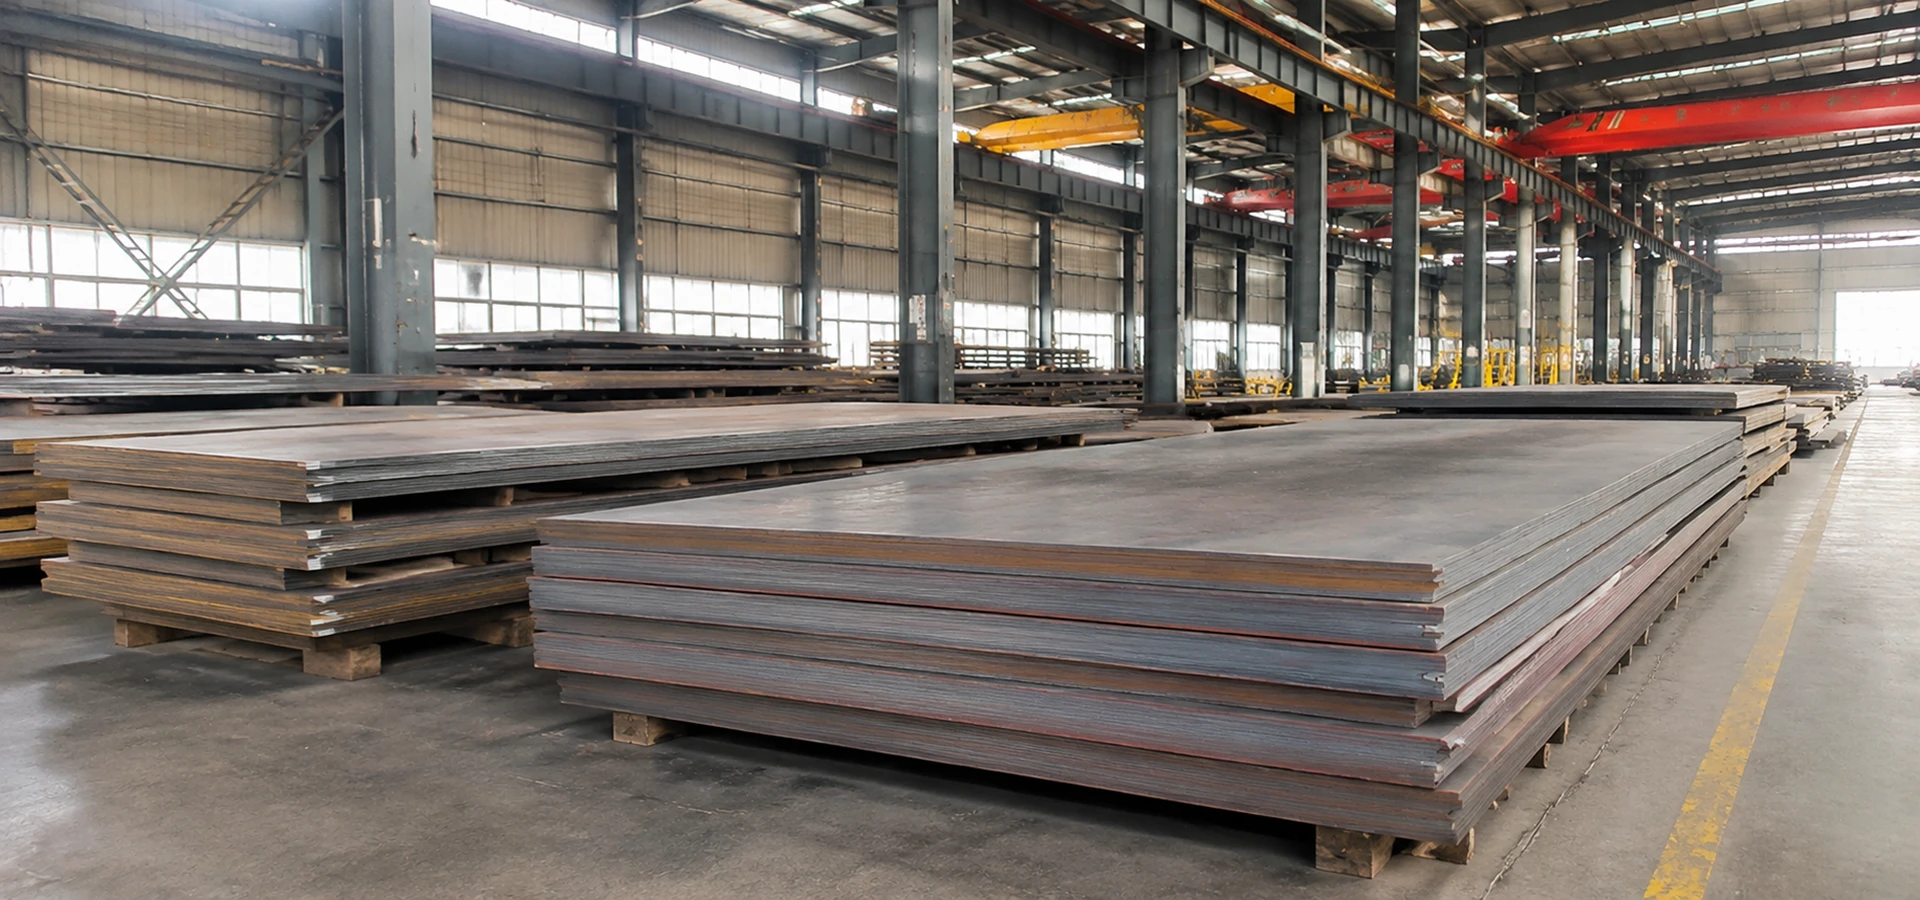
Confirm the nickel chemistry, heat treatment and the correct Charpy band alongside the grade name.
| Specification item | 09MnNiDR procurement requirement |
|---|---|
| Grade | 09MnNiDR — nickel-alloyed low-temperature pressure vessel steel |
| Current product standard | GB/T 713.3-2023 — specified low-temperature properties, alongside GB/T 713.1-2023 general requirements |
| Previous standard | GB/T 3531-2014 was fully replaced on March 1, 2024; legacy projects may name that edition explicitly. |
| Nominal thickness in grade table | 6–120 mm under the 09MnNiDR grade table; actual widths, lengths and available stock depend on the source mill. |
| Plate width and length | Mill production or stock dimensions confirmed against each RFQ; cut-to-length services subject to agreed tolerance. |
| Delivery state | Normalized (N) or Normalized + Tempered (N+T), as specified by the purchase contract. |
| Impact test | Charpy KV2 ≥60 J: −70°C for 6–80 mm, −60°C for >80–120 mm, subject to specimen and testing rules. |
| Base inspection documents | Producing mill test certificate, grade/heat identity, chemistry, tensile and impact test results. |
| Project additions | UT/NDT, supplementary chemistry, Z-direction properties, HIC, third-party witnessing and specified PWHT simulation when applicable. |
| Quantity and Incoterm | State pieces or MT, destination, requested shipping term and required delivery window. |
Product-property tables describe GB/T 713.3-2023 grade requirements. They are not a live stock list or a guarantee that every mill can supply every listed dimension.
Specify 09MnNiDR, thickness, plate size, tonnage and the required Charpy test temperature in one request.
Five thickness intervals from 6 mm through 120 mm, including the 80 mm impact transition.
Grade 09MnNiDR is grouped by nominal thickness for strength and toughness. The impact test temperature changes above 80 mm, even though the minimum specified energy remains 60 J. Use the thickness row corresponding to the nominal plate ordered; reported yield is lower yield strength ReL, or Rp0.2 when a distinct yield point is absent.
| Nominal thickness (mm) | Min. yield (MPa) | Tensile Rm (MPa) | Min. elongation (%) | Charpy requirement |
|---|---|---|---|---|
| 6–16 | 300 | 440–570 | ≥23 | −70°C / ≥60 J |
| >16–36 | 280 | 430–560 | ≥23 | −70°C / ≥60 J |
| >36–60 | 270 | 430–560 | ≥23 | −70°C / ≥60 J |
| >60–80 | 260 | 420–550 | ≥23 | −70°C / ≥60 J |
| >80–120 | 260 | 420–550 | ≥23 | −60°C / ≥60 J |
Reference: GB/T 713.3-2023 Table 2. The full material standard and GB/T 713.1 govern specimen selection, test orientation, reduced-size impact testing, retests and any agreed supplementary conditions.
Specify the actual heat chemistry and any project-specific alloy restrictions.
09MnNiDR has a specified nickel range of 0.30–0.80%, lower carbon and tighter phosphorus and sulfur limits than 16MnDR. Use the heat analysis on the actual mill certificate; product analysis deviations follow applicable GB/T 713.1 rules.
| Element | Heat-analysis requirement (%) | Procurement note |
|---|---|---|
| Carbon (C) | ≤0.12 | Heat analysis maximum |
| Silicon (Si) | 0.15–0.50 | Heat analysis range |
| Manganese (Mn) | 1.20–1.60 | Heat analysis range |
| Nickel (Ni) | 0.30–0.80 | Required heat-analysis range |
| Phosphorus (P) | ≤0.015 | Heat analysis maximum |
| Sulfur (S) | ≤0.005 | Heat analysis maximum |
| Molybdenum (Mo) | ≤0.08 | Heat analysis maximum |
| Niobium (Nb) | ≤0.040 | Heat analysis maximum |
| Nitrogen (N) | ≤0.012 | Heat analysis maximum |
| Aluminum, total (Alt) | ≥0.020 | Als / microalloy alternatives as specified |
If acid-soluble aluminum (Als) is used instead of total aluminum, Als is at least 0.015%. The aluminum acceptance rule also includes an exception when Nb+V+Ti ≥0.015%; verify the chosen mill route against the current standard.
State the alloy, carbon-equivalent or weldability limits and any product-analysis requirements in the RFQ.
Low-temperature impact acceptance depends on plate thickness and the certified mill test results.
Specified for 09MnNiDR from 6 through 80 mm. For >80–120 mm, the table specifies −60°C / 60 J. Confirm actual test specimens, orientation, coupon position and mill test record.
Base material-table condition for nominal plate thickness through 80 mm. Match the MTC to the ordered heat.
The thicker nominal plate band has a different baseline test temperature. Ask about enhanced −70°C testing if specified by the design.
Plate tests do not replace equipment-code material selection, weld and HAZ qualification or fabrication acceptance.
Match the mill process and final test values to the condition required by your vessel design.
GB/T 713.3-2023 lists 09MnNiDR in the normalized or normalized-plus-tempered delivery condition. Heat-treatment requirements are therefore central to the quotation and mill inspection plan.
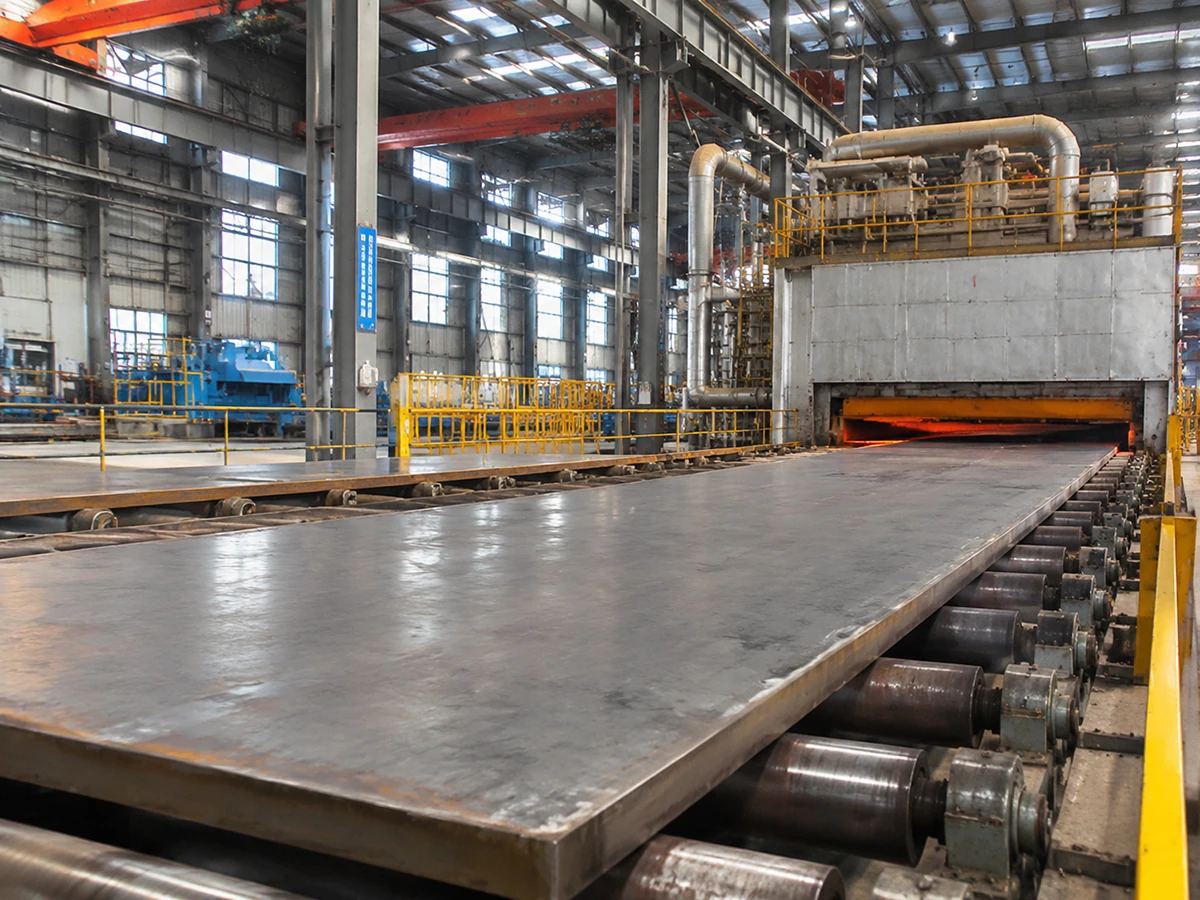
Compare baseline toughness, grade identity and approved equipment specifications before selecting the material.
| Material | Standard | Typical delivery | Impact acceptance route | Buying distinction |
|---|---|---|---|---|
| 09MnNiDR | GB/T 713.3-2023 | N / N+T | −70°C / 60 J ≤80 mm; −60°C / 60 J >80–120 mm | Mn–Ni vessel steel; low-temperature grade |
| 16MnDR | GB/T 713.3-2023 | N / N+T | −40°C / 47 J | C–Mn low-temperature pressure vessel plate |
| Q345R | GB/T 713.2-2023 | Project-approved rolling / heat treatment | 0°C / 41 J basic route | Different ambient-temperature pressure plate |
| ASTM A516 Grade 70 | ASTM A516/A516M | As-rolled / normalized by thickness & agreement | Impact by order / code | Separate ASTM material standard |
| ASTM A537 Class 2 | ASTM A537/A537M | Q&T | Impact by order / code | Separate ASTM heat-treated pressure steel |
Rows are a purchasing comparison, not an equivalence table. Material substitution requires the equipment designer or applicable code authority to approve strength, toughness, chemistry, weldability, thickness and heat treatment.
Plate selection depends on the design temperature, weld procedure and vessel approval.
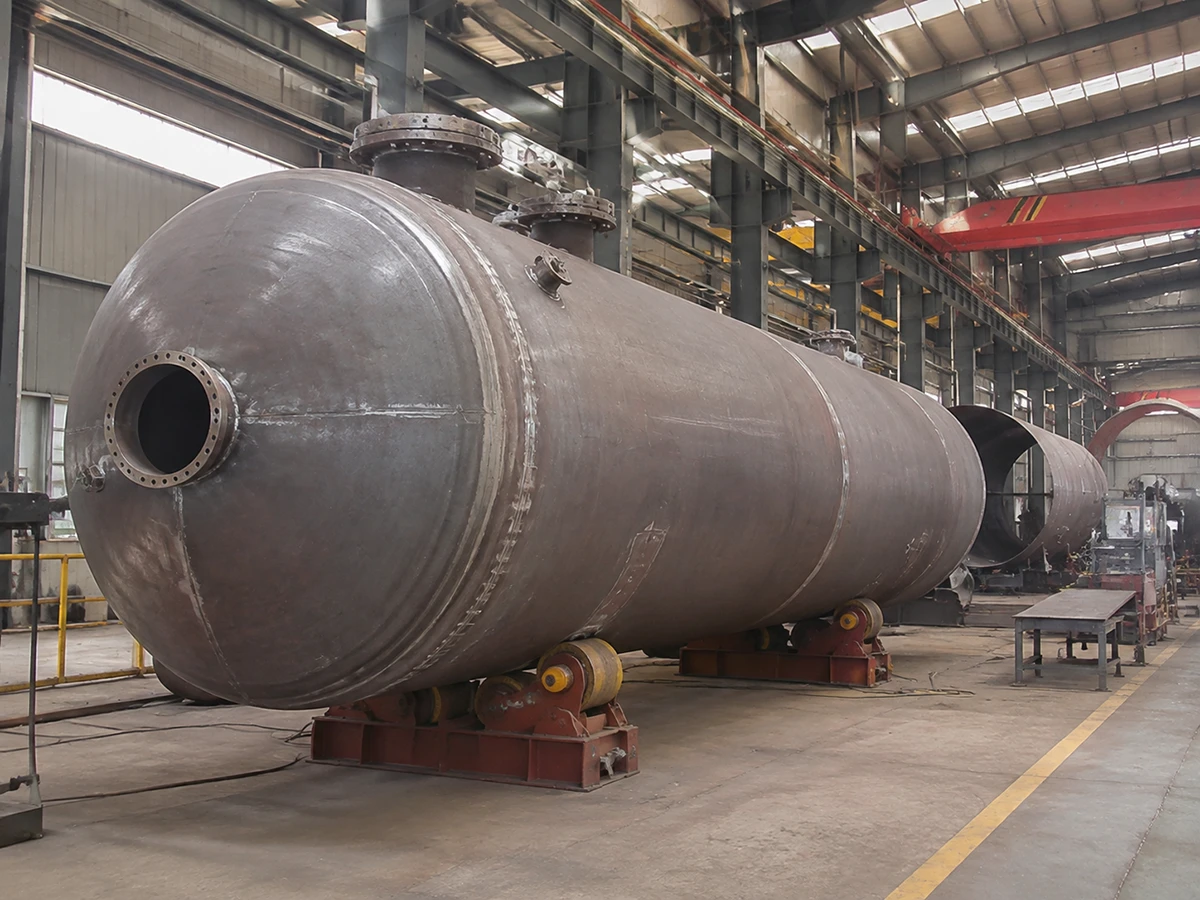
Shells, heads and heavy components using the specified 09MnNiDR low-temperature material route.
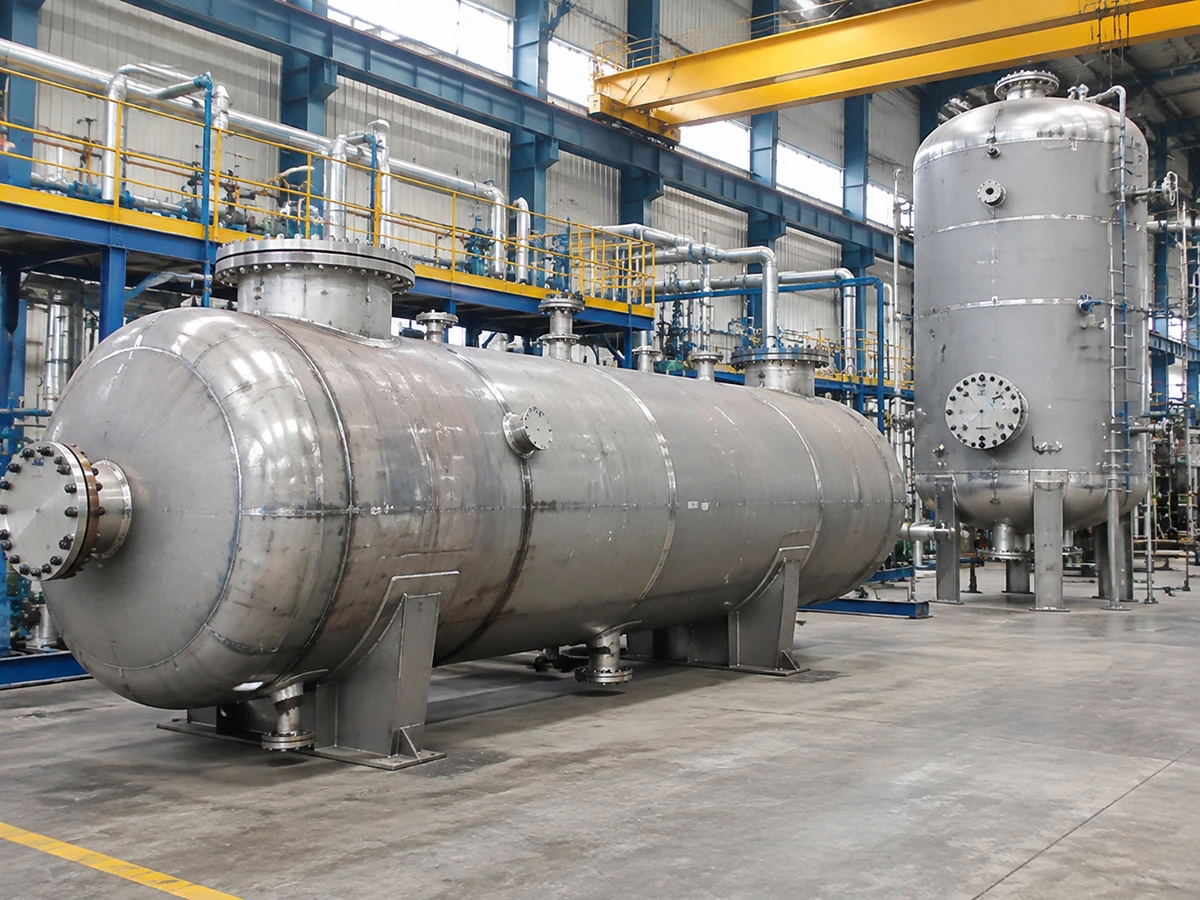
Equipment selected for cold-service conditions under the responsible design code and approval requirements.
Vessels designed for low-temperature fluid handling under applicable project codes.
Specified low-temperature plates for engineered pressure-containing assemblies.
Plate orders with traceable heat treatment and impact test documents.
Drawings, material standard edition and test records matched to the approved repair plan.
Applications are indicative. Final suitability for the design temperature, fluid, weld process and national pressure-equipment regulation is determined by the competent design and manufacturing teams.
Document the actual vessel fabrication route before material release.
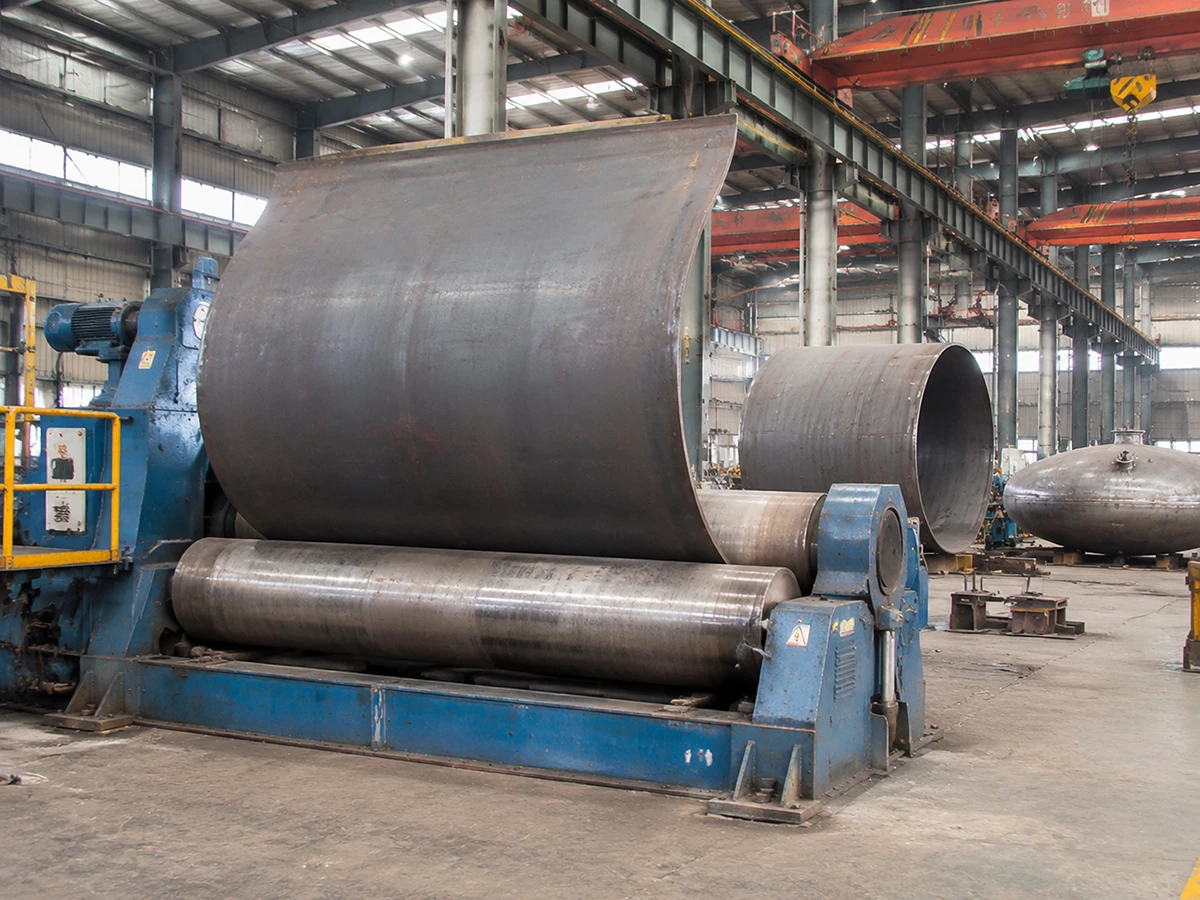
A low-temperature base-metal result must be supported by the applicable fabrication procedure, including weld metal and heat-affected-zone toughness.
A project-supply approach centered on material conformity and a clear purchase path.
Quote the specified GB/T 713.3 edition, 09MnNiDR material, nominal thickness band and required heat treatment.
Coordinate mill chemistry, tensile results and −70°C / −60°C Charpy records by heat and plate identity.
Check mill routes, stock plates and realistic lead times rather than implying every size is on hand.
Align cut sizes, material markings, packing, destination and commercial paperwork.
BAOSTEEL METAL company-wide operating figures: approximately 8 million MT annual output, 1 million MT regular inventory, 500,000 m² and 1000+ employees. These figures cover our broader steel operations and are not 09MnNiDR-specific capacity or ready stock.
A plate grade must be supported by a real mill route and a matching certificate.
We match the required plate thickness, delivery condition and inspection requirements against the producing mill and its actual manufacturing capability.
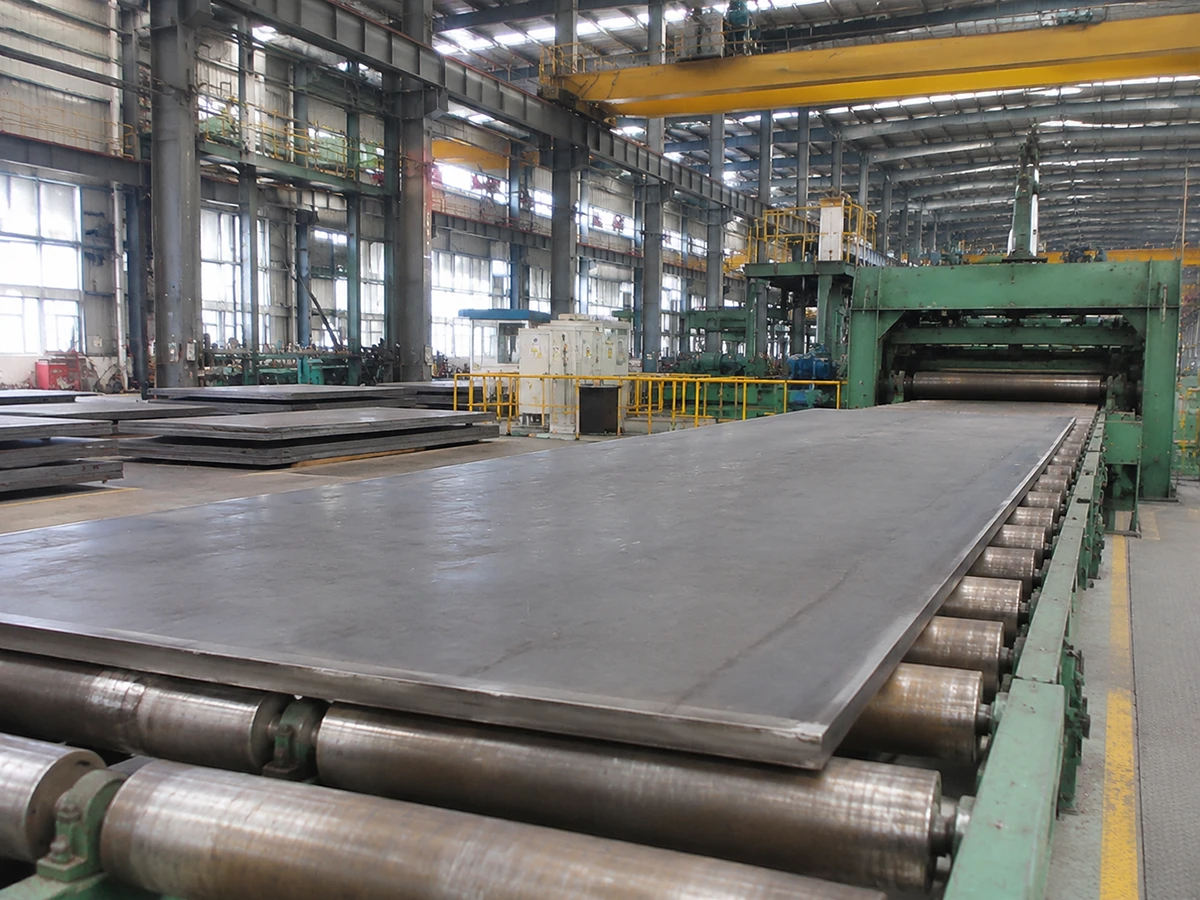
Quote from an actual mill or stock position and avoid assumptions about grade-specific inventory.
Provide thickness, width, length, pieces, destination and target delivery date.
Identify feasible ready stock or new plate production with N / N+T condition.
Agree Charpy, MTC, chemistry and any UT / HIC or third-party witness terms.
Review verified dimensions, delivery term, packing, schedule and price.
Send your material list to check stock plates, mill lead time and available certificates.
Source plate with traceable chemistry, heat treatment and correct temperature-based impact records.
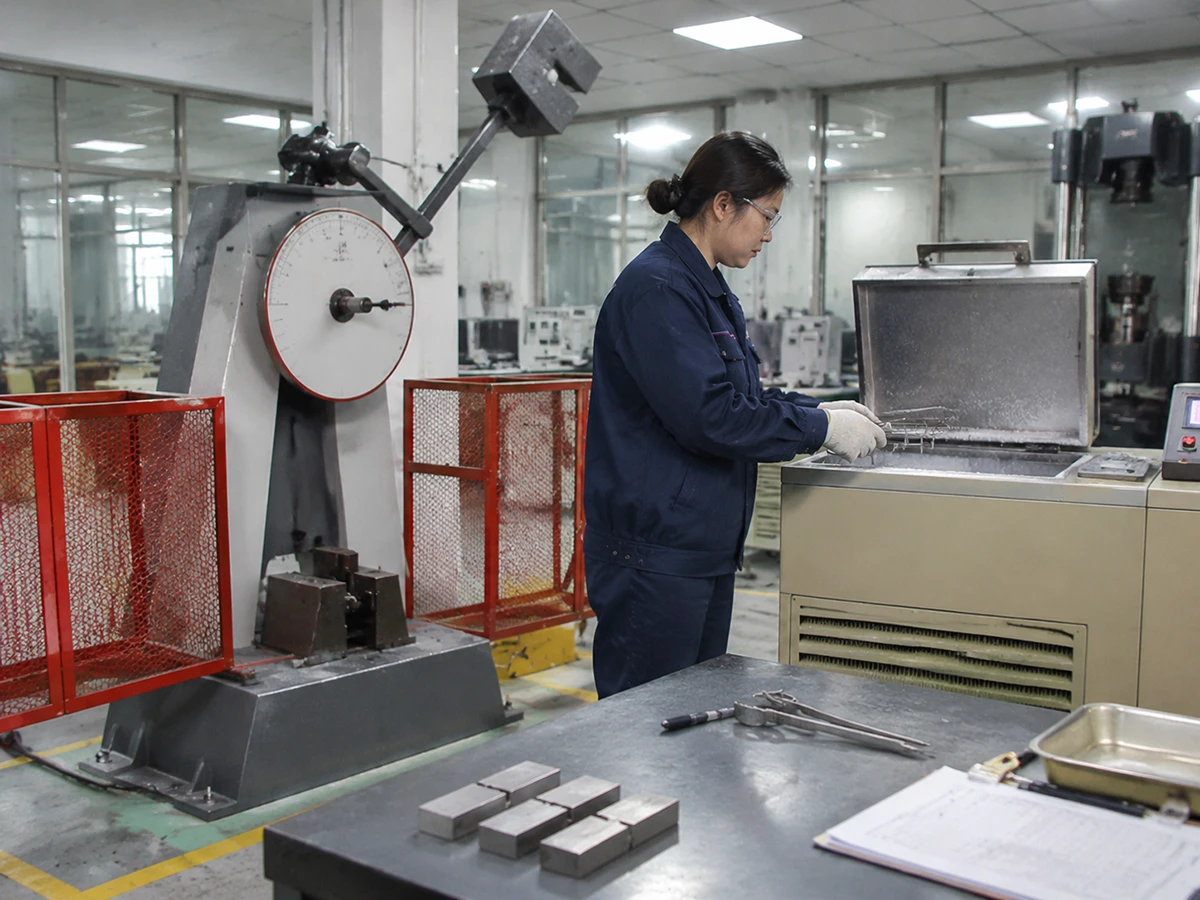
09MnNiDR material release depends on the producing-mill certificate, tested plate heat, nominal thickness and the applicable Charpy temperature band.
Select the right additional tests and acceptance criteria before rolling or dispatch.
Specify the scanning scope, test standard and acceptance class before quotation.
Sour-service requirements and applicable HIC/SSC test methods must be stated separately.
Discuss Z-direction testing and conditions when joint design or contract calls for it.
For >80–120 mm, request −70°C impact testing explicitly if required instead of assuming the base −60°C route covers it.
Plan witness hold points and the required document format ahead of mill release.
Identify any simulated fabrication heat cycle and the intended subsequent mechanical testing.
The base grade does not guarantee every supplementary service test. Project-specific requirements are priced and accepted as part of a documented purchase order.
Estimate shipping tonnage before requesting an actual mill quote.
Enter nominal plate dimensions in millimeters and a whole-number quantity. Density 7,850 kg/m³ is used for planning only.
Theoretical weight only; delivered mass follows actual dimensions and the applicable tolerance/packing rules.
Processing supports procurement; final component acceptance follows the equipment fabricator’s requirements.
Request simple processing around your plate supply. Retain heat traceability and any required testing plan after cutting.
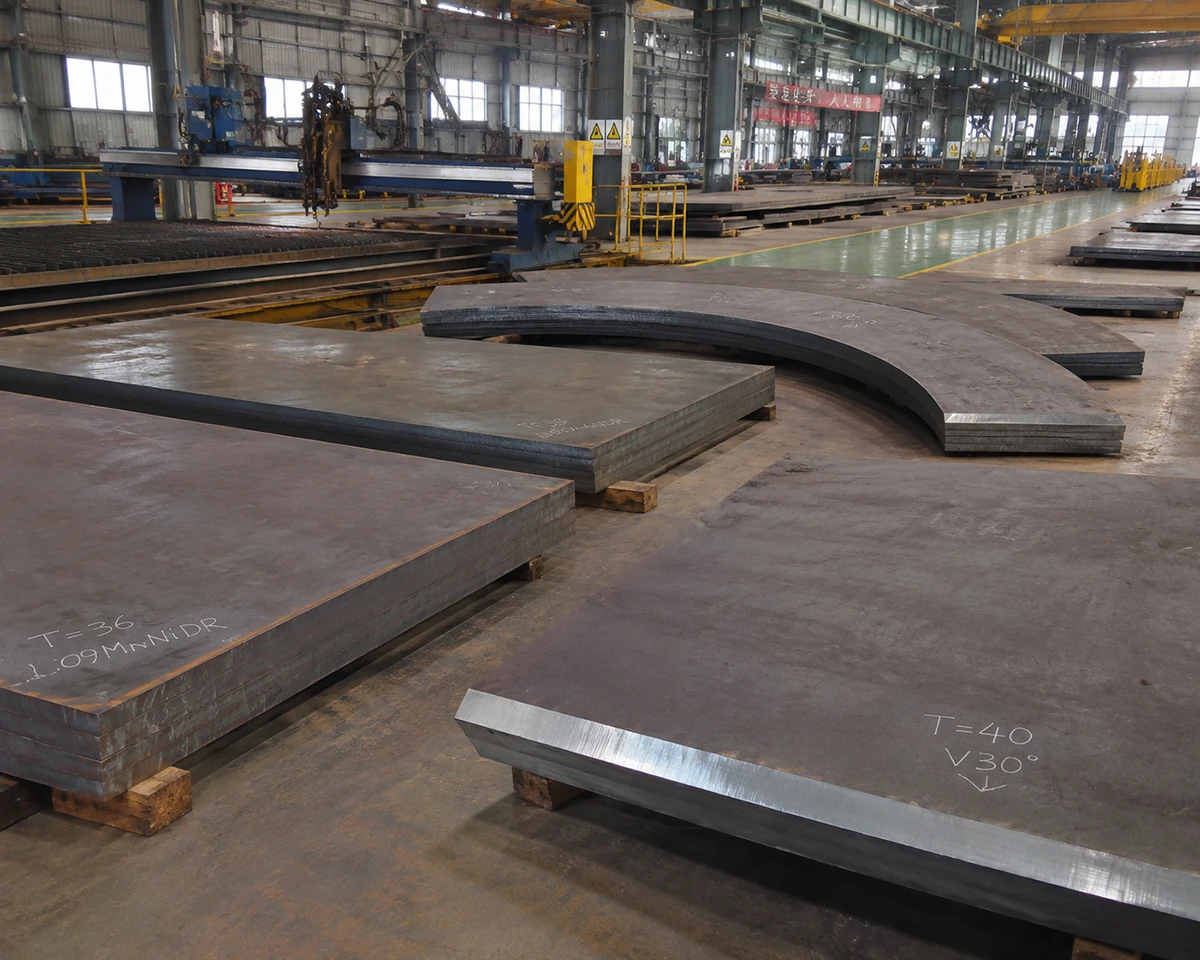
Specify DXF drawings, dimensions, tolerance and marking.
Match cut components to parent plates and certificates.
Identify UT / edge checks in the cutting schedule if required.
Keep receiving inspection straightforward with clear identifiers and document traceability.
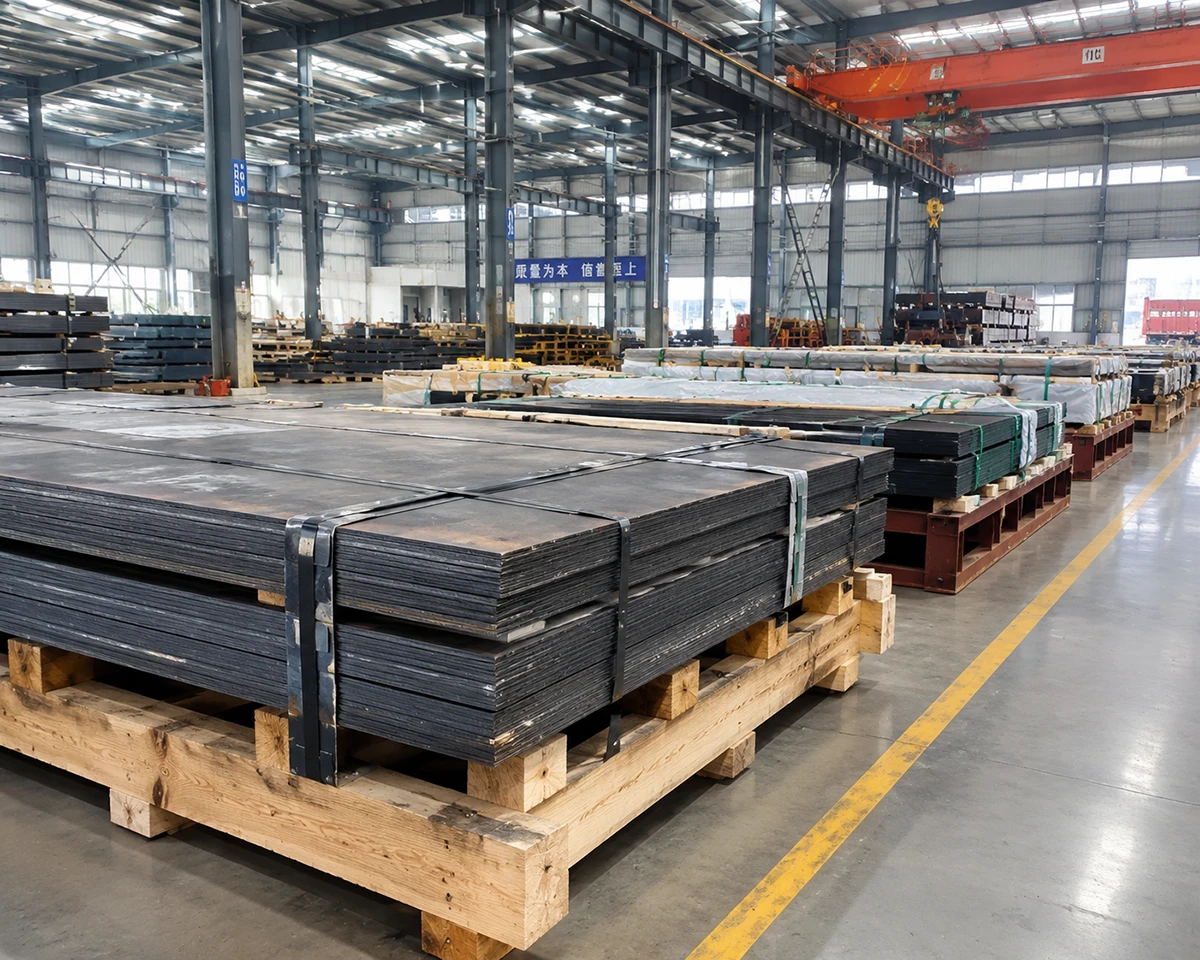
We coordinate suitable plate supports, steel strapping, marking, packing lists and shipping preparation with the agreed transport mode.
Use the source standard and design conditions to shortlist possible material systems.
All products have separate standard requirements. If a linked page remains an unpublished WordPress draft, publish it before activating the corresponding internal link.
Material identity, impact testing and documentation drive most project RFQs.
Clear answers to common questions about low-temperature plate, material standards, testing and export orders.
09MnNiDR is a manganese–nickel low-alloy steel plate for pressure equipment with specified low-temperature properties under GB/T 713.3-2023.
GB/T 713.3-2023, effective March 1, 2024, with applicable general requirements under GB/T 713.1-2023.
No. The base grade table specifies −70°C / 60 J for 6–80 mm, and −60°C / 60 J for >80–120 mm.
The minimum is 300 MPa at 6–16 mm, 280 MPa above 16–36 mm, 270 MPa above 36–60 mm, and 260 MPa above 60–120 mm.
Normalized (N) or normalized plus tempered (N+T), with any permitted special process route subject to agreement and certificate verification.
09MnNiDR has a heat-analysis nickel requirement of 0.30–0.80%; the actual measured chemistry should appear on the mill certificate.
Material substitution requires design authority approval for code, nominal thickness, chemistry, impact performance and weld/fabrication conditions.
Additional UT, HIC, through-thickness or independent inspection should be defined with methods and acceptance requirements in the order.
Request the producing-mill MTC with heat number, plate identity, chemical analysis, tensile properties, impact values and delivery condition, plus ordered supplementary reports.
Send thickness, width, length, quantity, N/N+T delivery state, required Charpy temperature, vessel code, document scope and destination.
Share the GB/T 713.3 grade and edition, thickness, dimensions, tonnage, normalizing condition, thickness-specific Charpy records, vessel code, destination and required delivery window. Receive a mill-verified technical and commercial response.
Send your required grade, dimensions, quantity and destination. Our team will review the inquiry.
