Global Steel Supply & Processing
Specify quenched-and-tempered carbon–manganese–silicon plate for welded vessels and qualified storage tank projects. We coordinate the exact plate thickness, strength class, heat-treatment record, MTC and optional inspection with the source mill before quotation.
Minimum yield is thickness-specific: 415 MPa through 65 mm, 380 MPa over 65–100 mm and 315 MPa above 100 mm within the applicable mechanical route.
A reliable pressure-vessel plate purchase starts with the precise class, mill heat-treatment route and acceptance documents.
| Buying Parameter | Specification / RFQ Guidance |
|---|---|
| Product identity | ASTM A537/A537M-20 Class 2 pressure vessel steel plate |
| Pressure-code route | ASME SA-537/SA-537M Class 2 only when ordered and certified by the producing mill |
| Mandatory condition | Quenched and tempered (Q&T), with traceable heat and tensile testing |
| Thickness bands | ≤65 mm / >65–100 mm / >100 mm; actual mill supply, size and testability to be confirmed |
| Plate dimensions | Width, length and thickness to mill production or confirmed inventory; A20/A20M tolerances as applicable |
| Surface and edges | Hot-rolled heavy plate finish, mill edge or cut/trimmed edges as specified |
| Required documents | MTC with grade, heat number, analysis, tensile tests and Class 2 condition |
| Optional examination | Charpy, ultrasonic, HIC, simulated PWHT and third-party witness by agreement |
The active 2020 ASTM text does not set one universal saleable maximum thickness: the ability to meet the mechanical-property requirements governs. Published Class 2 tensile-property bands include thickness above 100 mm; any exceptionally thick plate needs a mill-specific and design-code review.
Send dimensions, plate count, code edition, Q&T certificate wording and test plan to receive a source-specific proposal.
Use the correct yield/tensile range and 50 mm elongation requirement for your plate gauge.
For SI-based ASTM A537 Class 2 orders, the tensile-property requirement changes with nominal thickness. The 50 mm elongation minimum also changes beyond 100 mm. Apply the purchased standard edition and relevant ASTM A20/A20M elongation adjustments.
| Plate Thickness | Minimum Yield | Tensile Strength | Elongation in 50 mm |
|---|---|---|---|
| ≤65 mm | 415 MPa | 550–690 MPa | ≥22% |
| >65–100 mm | 380 MPa | 515–655 MPa | ≥22% |
| >100 mm | 315 MPa | 485–620 MPa | ≥20% |
A 25 mm plate falls in the ≤65 mm mechanical-property band. Specify Q&T and request actual measured yield and tensile values on the MTC.
An 80 mm plate uses the >65–100 mm band. Verify Q&T capability, plate flatness, Charpy specification and delivery lead time.
The mechanical-property table is a procurement reference, not the basis for approving grade substitution or vessel design stress. Engineering decisions remain under the governing code.
Identify the specification route and read real composition from the producing mill's MTC.
ASTM A537/A537M-20 defines its own heat-analysis limits. The Mn band is thickness-dependent, while product-analysis limits differ from heat analysis. Request the actual heat data and any carbon-equivalent restriction with the quotation.
| Element / Thickness Band | ASTM Heat Analysis | Ordering Note |
|---|---|---|
| Carbon (C) | ≤0.24% | Heat-analysis maximum |
| Manganese (Mn), ≤40 mm | 0.70–1.35% | Heat analysis; qualified alternative chemistry possible |
| Manganese (Mn), >40 mm | 1.00–1.60% | Heat analysis |
| Silicon (Si) | 0.15–0.50% | Heat analysis |
| Phosphorus (P) | ≤0.025% | ASTM specification maximum |
| Sulfur (S) | ≤0.025% | ASTM specification maximum |
| Copper (Cu) | ≤0.35% | Heat-analysis maximum |
| Nickel (Ni) | ≤0.25% | Conditional higher Ni option subject to the standard CEV rule |
| Chromium (Cr) | ≤0.25% | Heat-analysis maximum |
| Molybdenum (Mo) | ≤0.08% | Heat-analysis maximum |
A supplier may offer more restrictive phosphorus/sulfur or specific CEV values, but such mill-specific figures are not the universal A537 Class 2 limit. Permitted alternative Mn/Ni chemistry must comply with the carbon-equivalent conditions in the purchased standard.
Confirm the entire production route with the source mill before issuing the purchase order.
ASTM A537 Class 2 is quenched and tempered after rolling. The standard minimum tempering temperature is 1100°F [595°C]. Confirm the producing mill's Q&T procedure and certificate details for the ordered thickness.
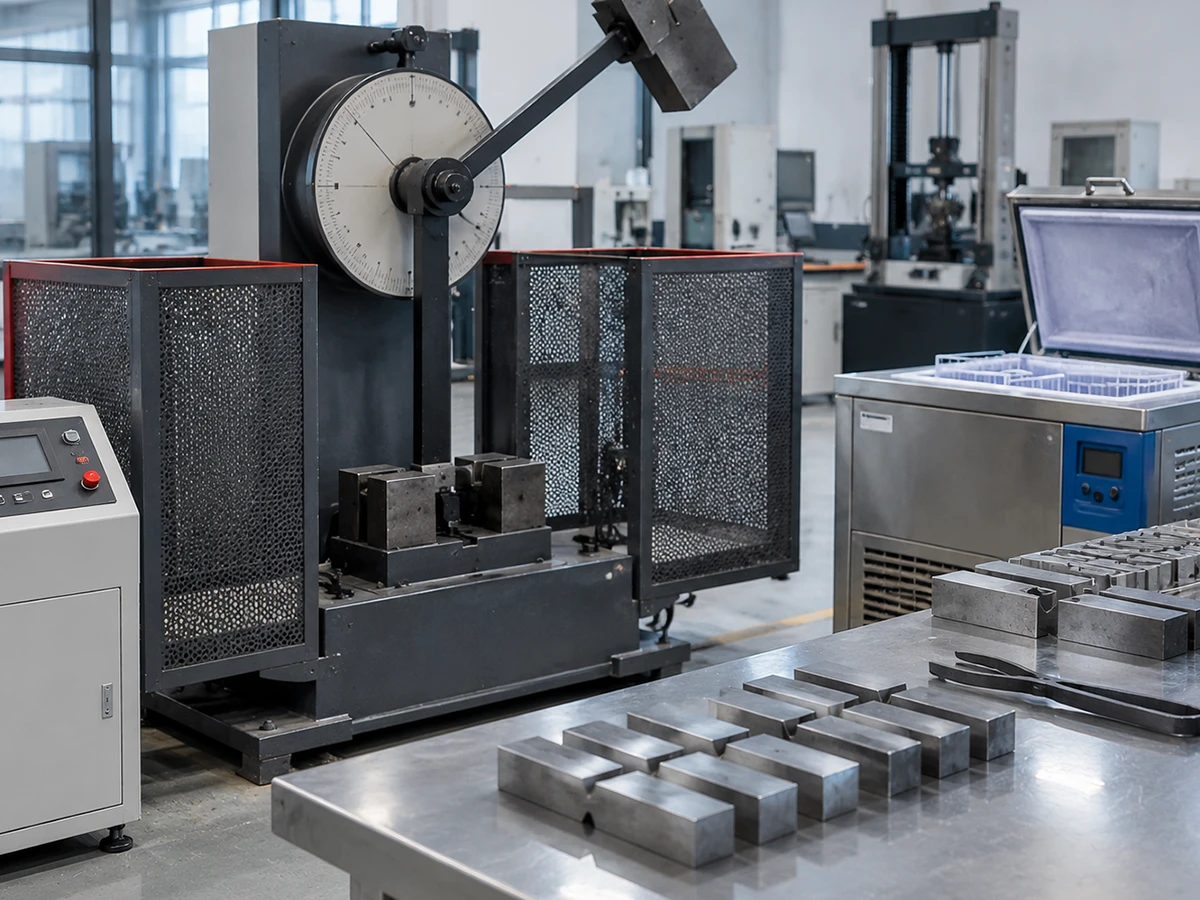
Include toughness conditions in the purchase schedule; obtain evidence against the actual producing mill and heat.
State the design minimum metal temperature and the actual required CVN test temperature for your pressure-vessel or tank code.
Provide the longitudinal/transverse test direction, minimum energy, specimen size, sampling and acceptance method.
Add supplementary Charpy testing to the purchase order and require heat-traceable results in the MTC or separate report.
Some mills offer −40°C / 41 J longitudinal Charpy as a typical supplementary option (for example, under A20 S5). This is not a universal base-material guarantee from the ASTM A537 Class 2 designation.
Include design temperature, requested test temperature, absorbed energy, test direction and acceptance level with your RFQ.
A537 Class 2 is the higher-yield quenched-and-tempered option in this comparison.
| Material | Min Yield at ≤65 mm | Tensile at ≤65 mm | Delivery Route |
|---|---|---|---|
| ASTM A537 Class 2 | 415 MPa | 550–690 MPa | Quenched and tempered — this page |
| ASTM A537 Class 1 | 345 MPa | 485–620 MPa | Normalized; separate specification |
| ASTM A537 Class 3 | 380 MPa | 550–690 MPa | Quenched and tempered; different yield strength class |
| ASTM A516 Grade 70 | 260 MPa | 485–620 MPa | A516-specific plate and heat-treatment rules |
Strength comparison is an aid to identifying the requested material, not an authorization to replace the design-approved grade. Confirm code, thickness, MDMT, impact testing and welding procedure before a substitution request.
The selected vessel standard and project drawings determine acceptance, not the broad end-use category.
Fabricated cylindrical shells and welded components where the design selects A537 Class 2 and requires Q&T material records.
Selected API 620 / API 650 designs subject to the actual project's permitted material grade, toughness and fabricator qualification.
Use only where design codes, test documents and fabrication requirements permit the material.
Agree the full Charpy temperature and acceptance package before relying on low-temperature performance.
An appropriate WPS/PQR and validated thermal cycle matter when pressure equipment is fabricated from quenched-and-tempered steel.
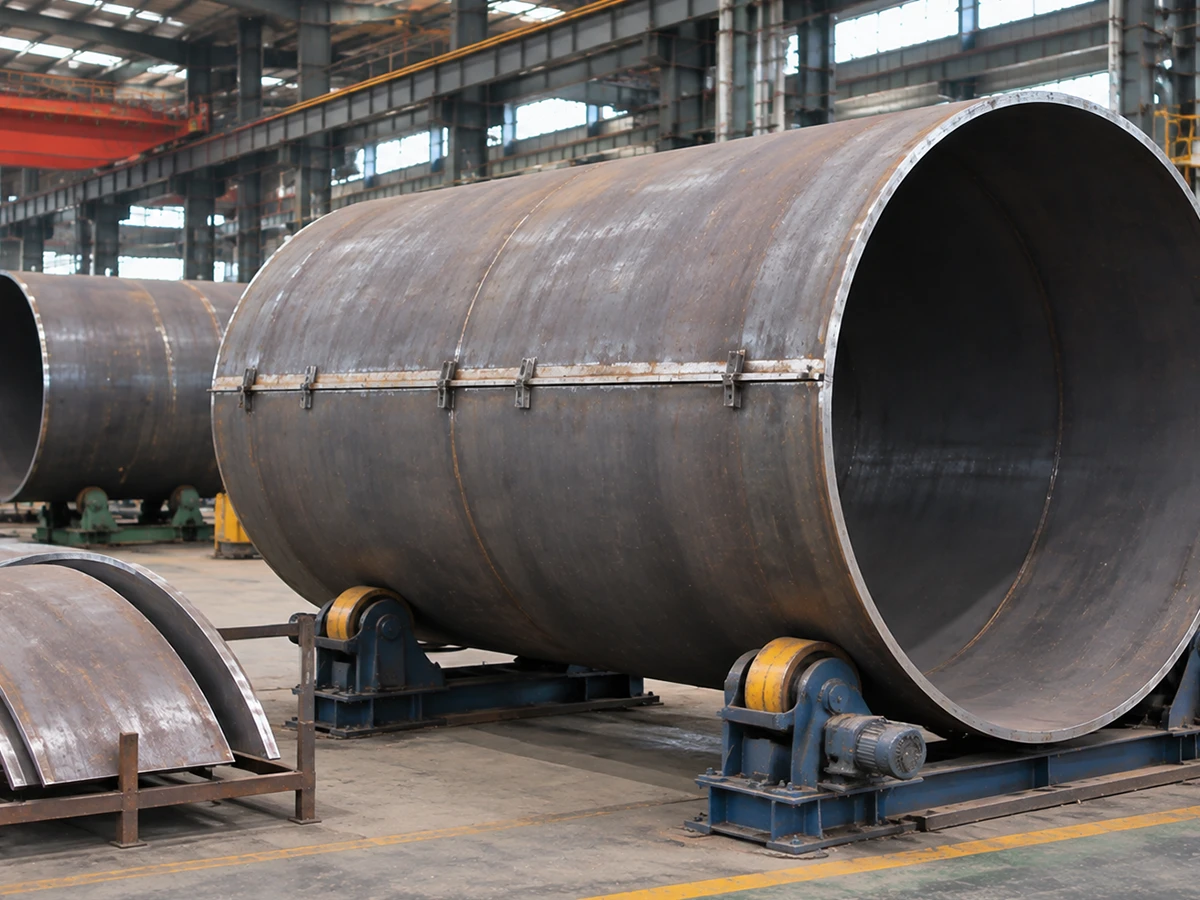
Welding, preheat, cold forming, hot forming and PWHT should be evaluated for the actual Class 2 heat, plate thickness, WPS/PQR and design code.
Purchase confidence comes from transparent mill routing, correct technical scope and fast quotation coordination.
Coordinate the exact A537 Class 2 plate designation, Q&T route and thickness-specific strength rather than a generic pressure-grade quote.
Agree the producing mill, MTC, final tensile report, inspection options and required certificate language.
BAOSTEEL METAL's company-wide steel operation has 8 million MT annual output, 1 million MT regular inventory and a 500,000 m² operating footprint.
Plan size checks, marking, packing, release inspections and shipping terms for overseas steel buyers.
These scale figures describe the company's entire steel business; they are not A537 Class 2-specific annual production figures or a live inventory guarantee.
The right heat-treatment line, mill test schedule and material identification must be matched to each plate order.
We check plate origin, finished thickness, heat-treatment sequence, mill documentation and production schedule when preparing your order.
Company-wide staffing exceeds 1,000 people across steel operations and related activities; a particular A537 Class 2 mill route is always confirmed separately.
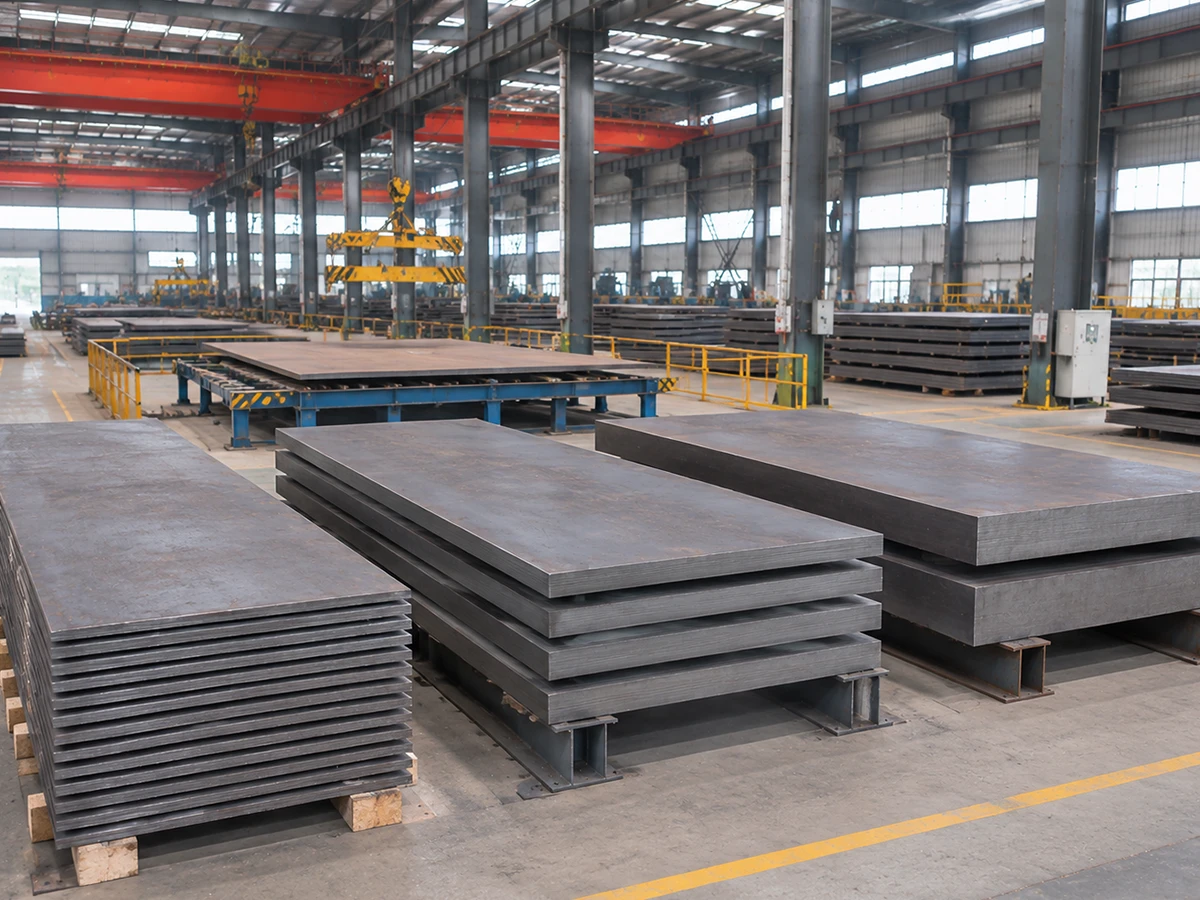
Company-wide steel stock is distinct from grade-specific A537 Class 2 inventory and ready-to-ship availability.
ASTM A537 Class 2 with documented Q&T, and ASME wording if required.
Thickness, width, length, cut quantity and overall tonnage.
MTC, Charpy, UT, third-party witnessing and required code acceptance.
Verified stock or rolling allocation, release and export freight.
Send your plate schedule and preferred shipping date. We will check source-mill Q&T and testing capacity for the exact dimensions.
The purchase-order document requirements are as important as the headline material grade.
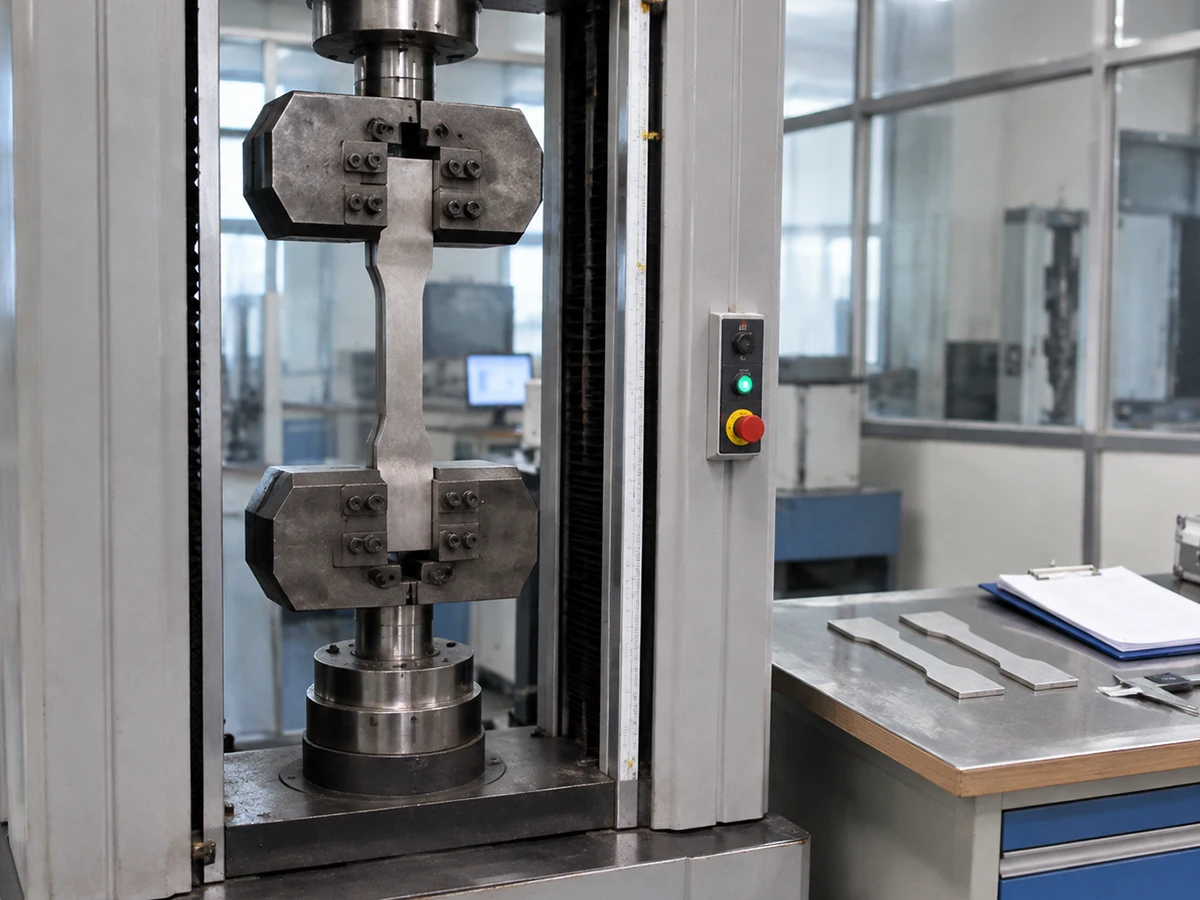
Ask for the actual producing mill's final material report showing the Class 2 condition and heat-based test values.
Write supplemental acceptance and witness requirements into the RFQ and purchase order.
Specify S5 where applicable plus temperature, energy, orientation, specimen size, sample count and any design-code conditions.
State inspection standard, scan coverage, acceptance class, reporting and inspection hold points.
Define precise procedures and limits when the vessel's service environment requires hydrogen-damage qualification.
Agree heat cycle, coupon treatment and retesting to reflect the intended fabrication thermal history.
Set agency, witness points, material records and pre-shipment release responsibilities.
Request ASME SA-537 Class 2 identification only where the actual material and mill documentation support that route.
UT, HIC, impact testing and third-party witnessing are not automatic certification features of every A537 Class 2 plate. Contract them with the producing mill before order release.
Get a quick theoretical tonnage before requesting a finished mill quotation.
Enter size in mm and piece count. Nominal steel density of 7,850 kg/m³ is used for procurement and freight estimates.
Theoretical estimate. Final delivered mass and dimensional tolerances follow the actual mill plate and packing list.
Keep the required steel identity and heat-treatment assurance through any requested cut-size delivery.
After checking plate dimensions and the effect of processing on Q&T properties, we can coordinate appropriate cropping, profile cutting and part marking.
Thermal cutting edges and subsequent heat exposure should be assessed by the fabricator for the final vessel specification.
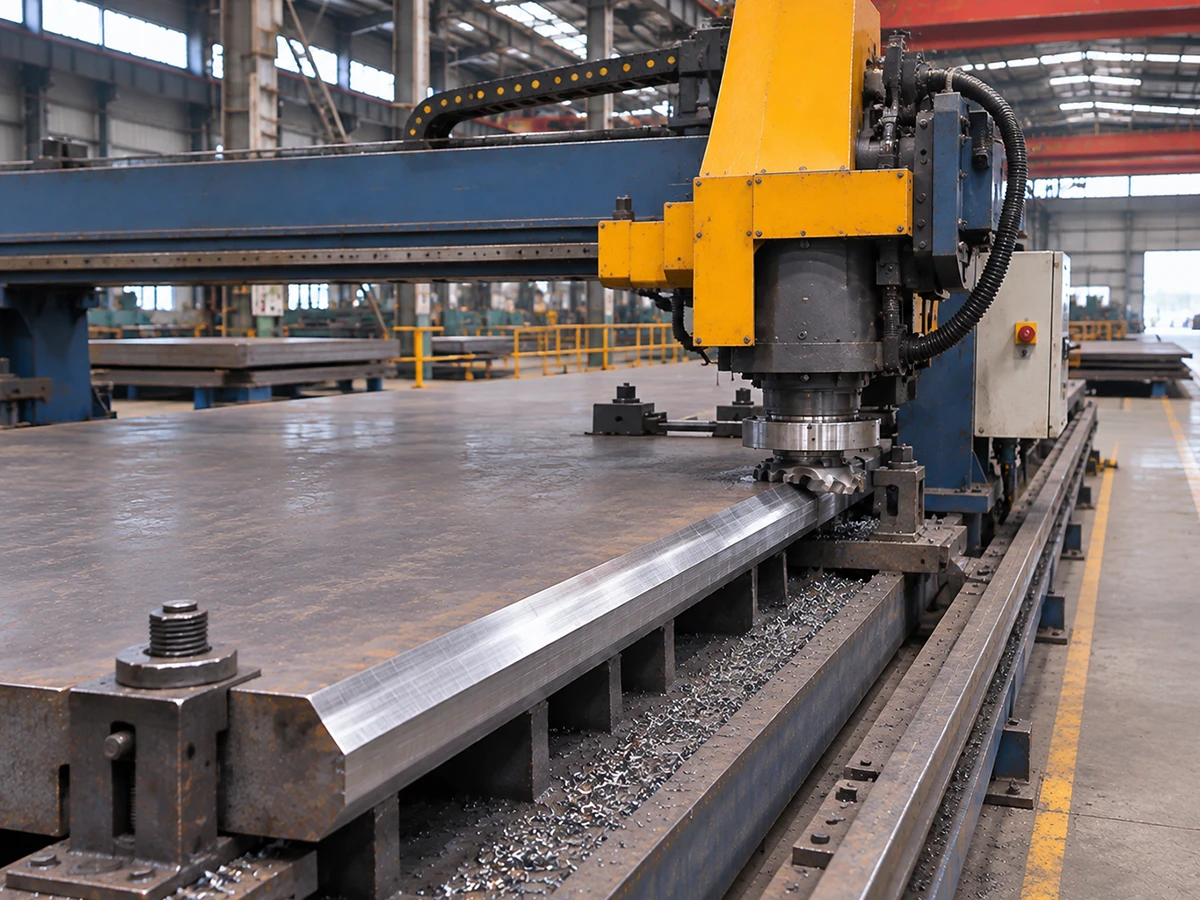
Coordinate mill material records and export packing so receiving teams can match plate identity quickly.
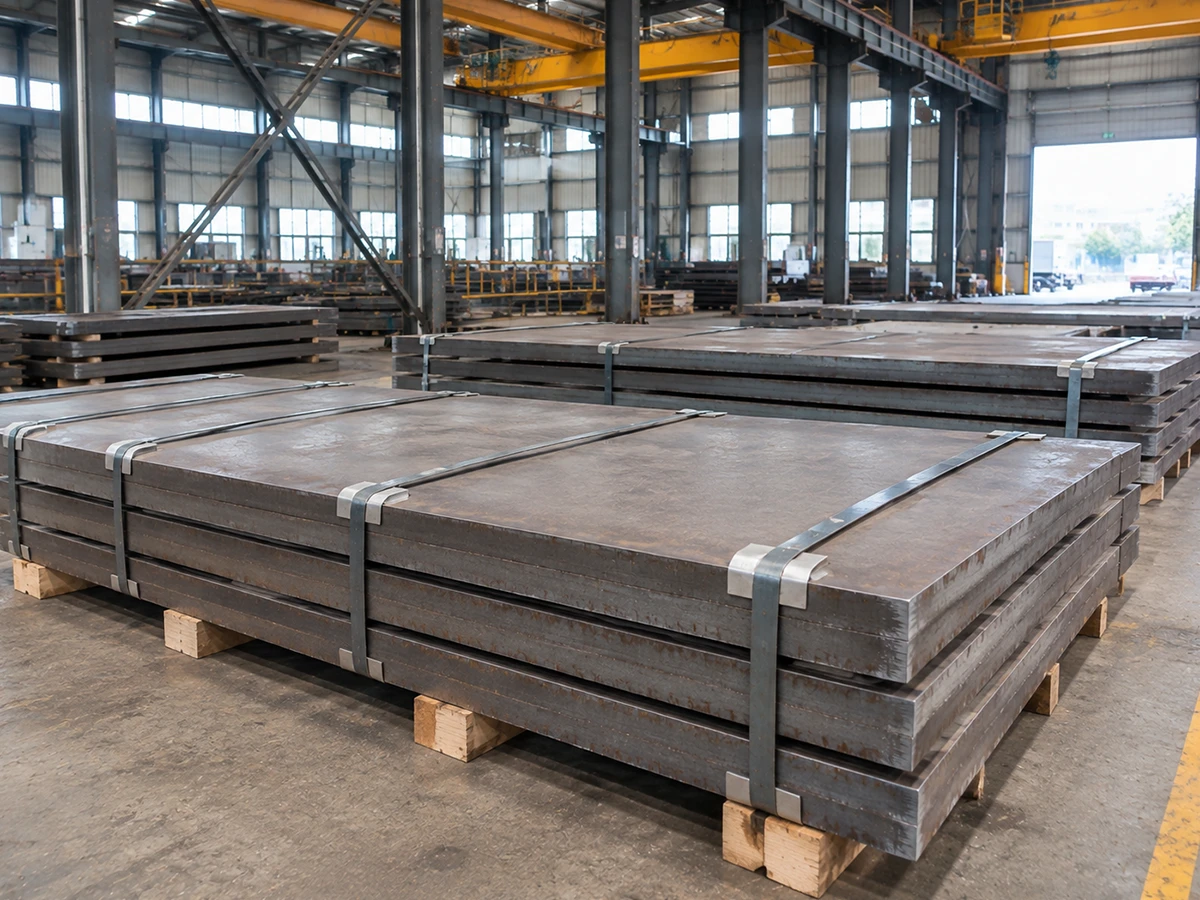
Set bundle weights, protection, lifting plan, heat marks, packing list and release inspections to fit your destination and port handling.
Compare normalized, quenched-and-tempered and alloy steel plate routes before finalizing the approved material.
The links help identify alternative pressure-steel product categories. ASTM, ASME and GB materials require independent design-code review and project approval before substitution.
Answers to the practical questions behind Q&T plate selection and purchase-order release.
Confirm the right heat treatment, strength band and inspection route before purchasing plate.
A quenched-and-tempered carbon–manganese–silicon pressure-vessel steel plate specified under ASTM A537/A537M. It is used only where the equipment design approves that material and test schedule.
Class 1 is normalized; Class 2 is quenched and tempered. At ≤65 mm, Class 1 requires at least 345 MPa yield while Class 2 requires at least 415 MPa.
For ASTM A537 Class 2 in the SI route, a plate over 65 mm through 100 mm requires at least 380 MPa yield strength and 515–655 MPa tensile strength.
The 2020 standard includes a >100 mm tensile-property band. A specific thick-plate offer requires mill confirmation that final dimensions, Q&T and mechanical tests can satisfy the order.
No. Class 2 is quenched and tempered. If the project requires normalized A537 plate, check whether Class 1 is the correct design-approved designation.
No universal base guarantee is implied. That is a published example of a supplementary mill toughness option; specify your own test conditions and acceptance level in the order.
ASTM A537 Class 2 has a minimum tempering temperature of 1100°F [595°C]. The source mill must confirm its actual Q&T process, finished condition and MTC.
Specify the ASME designation and edition at the inquiry stage. Any ASME or dual certification must be supported by the actual material, producing mill and documentation.
A qualified WPS/PQR, consumables, preheat and fabrication heat cycles are determined by the actual material, thickness and design code. Request simulated PWHT tests where needed.
These are project-specific additions. Share the test standard, acceptance criteria, sampling, inspection agency and witness points with your RFQ.
Send A537 Class 2, Q&T, plate sizes, piece count, code edition, MTC and supplemental tests, delivery date, destination and packing requirements.
Send your required grade, dimensions, quantity and destination. Our team will review the inquiry.
